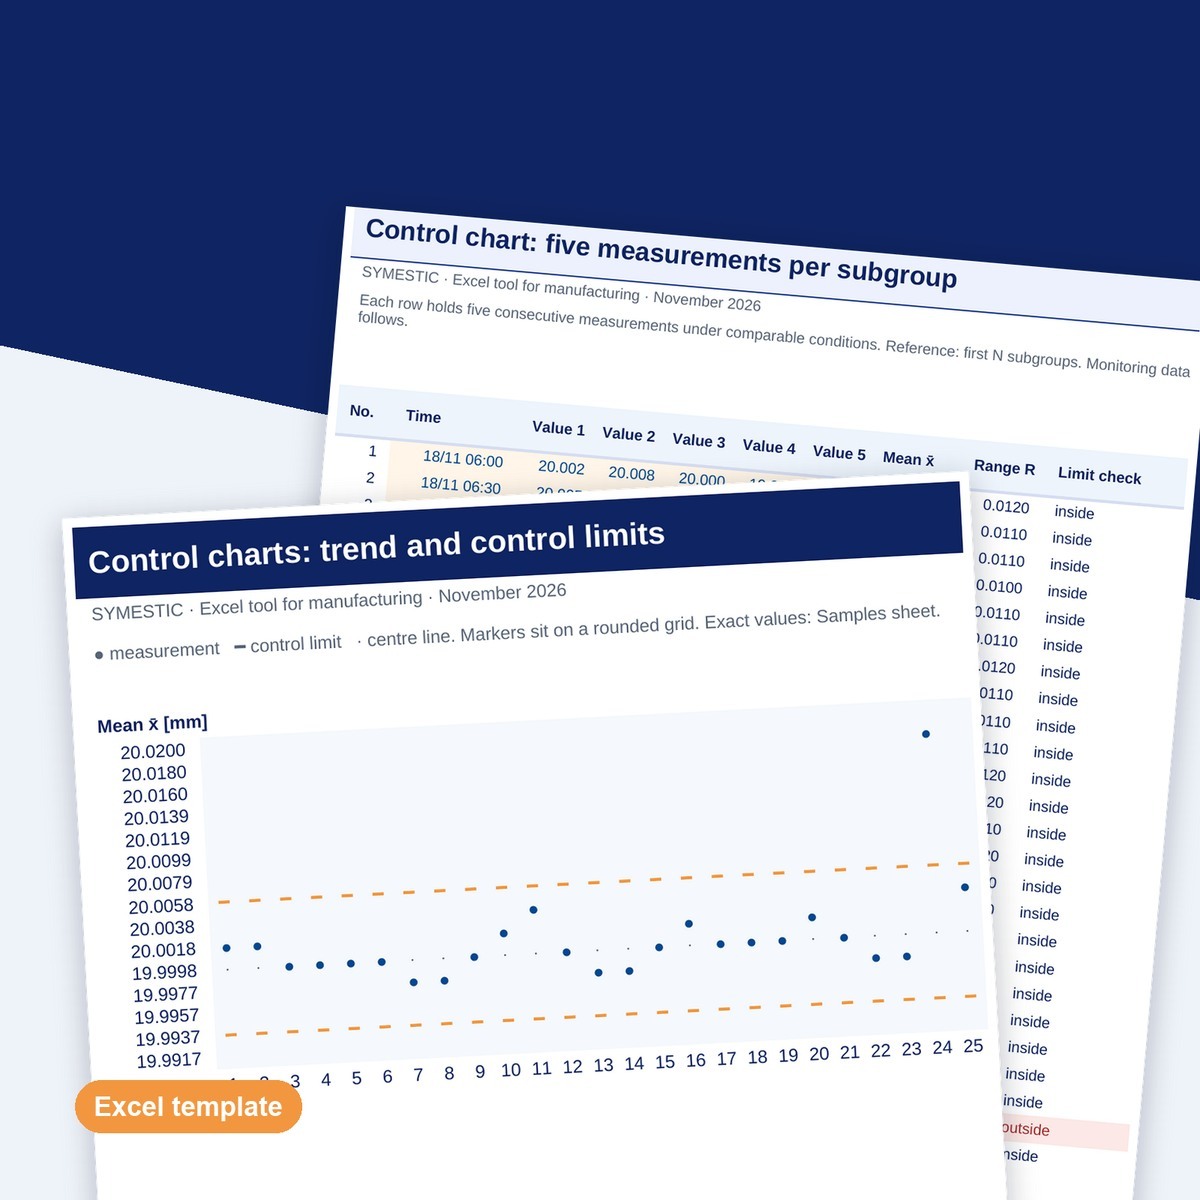
Control limits are statistically calculated boundaries on a control chart that separate normal process variation (common cause) from abnormal variation (special cause). They are set at ±3 standard deviations (σ) from the process mean, capturing 99.73 % of expected values when the process is stable.
Any data point outside these limits signals that something has changed, not that a product is defective. This distinction matters: control limits describe what the process does. Specification limits describe what the product must be.
Figure: Points inside the ±3σ control limits show common cause variation. A point outside signals a special cause in the process, not a defective part.
How are control limits different from specification limits?
This is the most common confusion in SPC. Mixing them up leads to either false alarms or missed process shifts. The table below shows the difference:
Dimension
Control limits (UCL / LCL)
Specification limits (USL / LSL)
Source
Calculated from process data (the voice of the process)
Defined by engineering, customer or regulation (the voice of the customer)
Purpose
Detect process instability: is the process behaving differently?
Judge product conformance: is the part within tolerance?
Formula
UCL = X̄ + 3σ; LCL = X̄ − 3σ
Set externally (e.g. 25.0 mm ± 0.1 mm)
Changes when…
Process improves or deteriorates (recalculated)
Customer or design requirements change
A point outside means…
Investigate the process: a special cause is present
Reject/rework the part: it does not conform
A process can be in statistical control (all points within control limits) and still produce defects if the natural process spread is wider than the specification window. That gap is measured by process capability (Cp/Cpk), a related SPC concept.
Conversely, a point inside specification limits can still signal a control limit violation, meaning the process is drifting even though parts still pass.
How are control limits calculated?
Control limits are derived from your own process data, never copied from another line or a textbook. The formula depends on the chart type. Below are the three most common control charts used in discrete manufacturing:
A₂, D₃, D₄ are constants determined by subgroup size (n). For n = 5: A₂ = 0.577, D₃ = 0, D₄ = 2.114. These values come from standard SPC factor tables and assume normally distributed data.
You need at least 20–25 subgroups of stable data before calculating meaningful control limits. Fewer subgroups mean the limits reflect noise, not the real process.
What are the Nelson rules for control chart interpretation?
A single point outside UCL or LCL is the most obvious signal. But control charts reveal process shifts before a limit violation occurs, if you apply pattern rules. The most widely used set:
Rule 1: 1 point beyond 3σ (classic out-of-control signal)
Rule 2: 9 consecutive points on the same side of the center line (process shift)
Rule 3: 6 consecutive points steadily increasing or decreasing (trend)
Rule 4: 14 consecutive points alternating up and down (over-adjustment or fixture issue)
In practice, Rule 2 is the one that catches real process drift earliest. A machine tool losing bearing preload will show 7–8 consecutive points above the mean before a single point crosses the UCL.
How does an MES automate control limits in production?
Manual SPC (sampling parts, writing values on paper charts, calculating limits by hand) still exists in many plants. It is slow, error-prone, and gives insight hours or shifts after the deviation occurred. A modern MES changes this:
Automatic data capture: Process parameters (temperature, pressure, force, cycle time) are read from the PLC via OPC UA or digital signals. Nobody enters values by hand, so there are no transcription errors.
Process stability: Control limits and Cp/Cpk are calculated from production data for each process parameter.
Context correlation: The MES knows which order was running, which material batch was loaded, which operator was on shift. A control limit violation then reads "point above UCL during order 47832 on machine 12 with material lot 2026-04-A3" instead of just "point above UCL." That context turns a chart signal into a root-cause investigation.
SYMESTIC's process data module captures SPC-relevant parameters in real time and correlates them with OEE, downtime and quality data.
FAQ
What happens when a point falls outside control limits?
Stop and investigate. A point beyond UCL or LCL means a special cause is present: something changed in the process (tool wear, material variation, setup error). It does not automatically mean the product is defective. Find the assignable cause, correct it, and verify that subsequent points return within limits before resuming normal production.
How often should control limits be recalculated?
After any confirmed process change: new tooling, material change, machine rebuild, or after a successful improvement project (kaizen). Never recalculate limits just to "widen" them so that out-of-control points disappear. That defeats the purpose. Limits reflect the real process capability. If capability improves, limits tighten. If it worsens, you fix the process, not the chart.
Can control limits be applied to OEE or downtime data?
Yes. Individual-X / moving-range (I-MR) charts work well for single-value data like shift OEE, hourly output or downtime duration. A shift OEE that violates the LCL triggers the same investigation protocol as a dimensional measurement beyond the UCL: something changed, so find out what.