




Contents
2.7 kWh per part one week. 3.4 kWh per part the next. Same machine, same product, same shift pattern. The plant manager only noticed because we'd built the dashboard that showed him — three months earlier, the same drift would have been invisible until the quarterly energy bill arrived and someone went looking for an explanation that no longer existed in any data anyone could reconstruct.
This is the part of smart energy management that almost every vendor pitch in 2026 skips: the absolute kWh number on a dashboard is not actionable. It tells you what you used; it does not tell you whether what you used was reasonable. The number that drives every real decision — keep the line, retool it, scrap it, schedule it differently, run it on a different shift, charge the customer more — is kWh per produced unit. And that number does not exist on any energy monitoring platform that doesn't know what was produced.
What is smart energy management, in one honest definition?
Smart energy management is the use of real-time energy measurement, production-context binding, and automated analysis to convert energy from a fixed-cost line on the P&L into a per-unit operational variable that can be optimised, attributed, and benchmarked across machines, products, and shifts.
That definition does most of the work. The "smart" word is doing less than the "production-context binding" phrase. An energy monitor without production context is a more sophisticated electricity bill. An energy monitor with production context is a manufacturing decision tool. The technology is the easy part; the data plumbing underneath is the difference.
Why kWh per part is the only number that matters
Take the same plant — a mid-sized injection moulding operation, 40 machines, three shifts — and look at three different energy numbers it could quote:
| Number | What it tells you | What it doesn't |
|---|---|---|
| Total monthly kWh | The size of the bill | Whether it was reasonable for what you produced |
| kW per machine over time | Where the demand peaks | Whether the peak was productive or wasted |
| kWh per produced unit | Whether energy spent created value | Almost nothing — this is the actionable number |
The worked calculation looks like this. Machine 17 ran an order for 8 hours, drew an average of 42 kW, produced 980 good parts. Energy per part: (42 × 8) ÷ 980 = 0.343 kWh/part. The same machine ran the same product the following week — 8 hours, 38 kW average, 720 parts. Energy per part: 0.422 kWh/part. The absolute energy use went down. The energy per part went up by 23%. The first number says the plant used less electricity. The second number says the plant got significantly less for what it used. Only the second is a decision.
This calculation cannot be done by an energy monitoring platform alone. It requires three data sources to meet at the same point: a power measurement (utility-grade meter or CT clamp), a production count (PLC tag, vision system, or counter), and an order context (which product was on which machine at which time, from the ERP or MES). The vast majority of "smart energy management" deployments I see in 2026 connect the first; the better ones get to the second; almost none of them close the third without a real production data layer underneath.
Where energy actually disappears in a typical plant
Twenty-five years of customer site visits has produced a fairly stable picture of where the energy that doesn't end up in a finished product actually goes. The pattern is more uniform across industries than people expect:
- Idle consumption
- Equipment energised but not producing — between orders, during changeovers, during breaks, on weekends when nobody powered things down. Typically 15–30% of total plant consumption in discrete manufacturing. Almost entirely invisible without per-machine measurement and production-state context.
- Compressed air leaks
- The single most expensive utility in most plants and the one with the worst loss profile. Industry averages put leak losses at 20–30% of total compressed air production. A 3 mm leak at 7 bar costs around €2,500/year at industrial electricity prices. Most plants have dozens.
- Wrong-shift production
- Energy-intensive operations running during peak-tariff hours (typically 09:00–20:00 in Germany) when they could have been scheduled for night-shift or weekend windows at 30–50% lower energy cost. Not a technology problem; a scheduling problem that energy data makes visible.
- Drift on baseline-consuming equipment
- HVAC running when nobody's there. Furnaces held at temperature longer than the next batch needs. Cooling systems sized for peak load running at peak load constantly. Dust extraction never throttled. These don't fail dramatically — they drift, and the drift compounds for years until someone instruments and notices.
What unites these four is that none of them is solved by buying an energy monitoring platform. They are solved by an energy monitoring platform that knows what production was happening at the time, attributes the consumption to it, and surfaces the gap between what should have been used and what was. That requires the production data infrastructure first, the energy layer second.
What a credible smart energy management implementation actually delivers
Setting aside the marketing framing — "AI-powered," "carbon neutrality," "digital twin" — the realistic outcomes from a properly implemented smart energy management programme in a typical mid-sized discrete manufacturing plant:
- 5–10% reduction in total energy consumption within the first 12 months, primarily from eliminating idle consumption and compressed air leaks once they become visible. This is the easy win and the one that funds everything else.
- 10–20% reduction in peak-tariff exposure within 6–18 months, from rescheduling energy-intensive work to off-peak windows. Pure planning gain, no equipment investment required.
- Per-product energy attribution that makes margin discussions honest — many products turn out to be less profitable than thought once their actual energy footprint is loaded in, and a few turn out more profitable. Both directions matter for pricing and product-mix decisions.
- Equipment health early-warning signal from energy drift — a motor drawing 8% more than its baseline for the same output is a maintenance signal months before it fails. Not the primary purpose of energy monitoring, but a real secondary benefit if the data is granular enough.
- CSRD/ESG reporting at the line-item level rather than as an annual estimate. Increasingly not optional in Europe; the reporting becomes a by-product rather than a project.
What it does not deliver — and what every honest practitioner has to be clear about — is the 30%+ savings figures that appear regularly in vendor pitches. Those numbers usually exist on greenfield projects with major equipment replacement bundled in, or against pathologically inefficient baselines. A reasonably-run plant with current equipment, doing the work properly, will see 5–10% in year one and further gains in year two as the harder optimisations get tackled. Anyone selling you 30% in a brownfield context against a normal baseline is selling you something else.
What people object to
"Our energy bill isn't that big — it's not worth the effort." This is the most common objection and it's almost always wrong, in two directions. First, the relevant comparison is not energy bill vs. project cost; it's the project's blended return across energy savings, peak-tariff avoidance, equipment-drift detection, and ESG reporting cost avoided. The energy savings alone usually carry the case for plants with annual electricity spend above €200k; below that threshold, the supporting benefits often tip it. Second, the energy bill matters less than its volatility — plants with electricity spend that swings ±20% quarter-on-quarter without explanation are taking margin risk that smart energy management eliminates whether or not it reduces the average.
"We don't need to install meters everywhere — we have a main meter." The main meter answers the wrong question. It tells you the total. Smart energy management requires per-machine or per-line measurement because the optimisable behaviours happen at that resolution. The good news is that sub-metering in 2026 is dramatically cheaper than it was even five years ago — Class 0.5 CT-based sub-meters cost €150–€400 per machine including installation, and a typical plant of 50 machines can be fully sub-metered for less than the cost of a single new piece of production equipment. The economics are not the obstacle; the perception that they are is.
"AI will figure out the optimisation automatically." Eventually, in some scoped applications, yes — anomaly detection and demand-response automation are real. But AI applied to energy data without production context produces the same hallucinations as AI applied to anything without context: confident, plausible, wrong. The order in 2026 is unchanged from what it was three years ago: instrument first, contextualise second, automate third. Skipping the middle step in pursuit of the third is the most expensive mistake in this space.
If you are evaluating smart energy management as a standalone project, the more useful frame is to look at it as an extension of your production data infrastructure. The reason SYMESTIC customers tend to get clean kWh-per-part numbers without a multi-month integration project is that the production-context layer — order, product, machine state, shift, operator — already exists in Process Data and surfaces in Production Metrics. Adding energy measurement on top of that is connecting one more signal type to a pipeline that already knows what to do with it. The same approach extends to compressed air, gas, water, and steam if those are material to your operation. If the production data infrastructure isn't there yet, that's the project to do first; energy attribution becomes a feature rather than its own initiative.
See also: OEE · MES · Data-driven manufacturing · Digital manufacturing platform · Industrial IoT · Predictive maintenance · Sustainability in manufacturing · CSRD reporting · Scope 1/2/3 emissions · Peak load management · Process Data · Production Metrics.
ExcelFree download
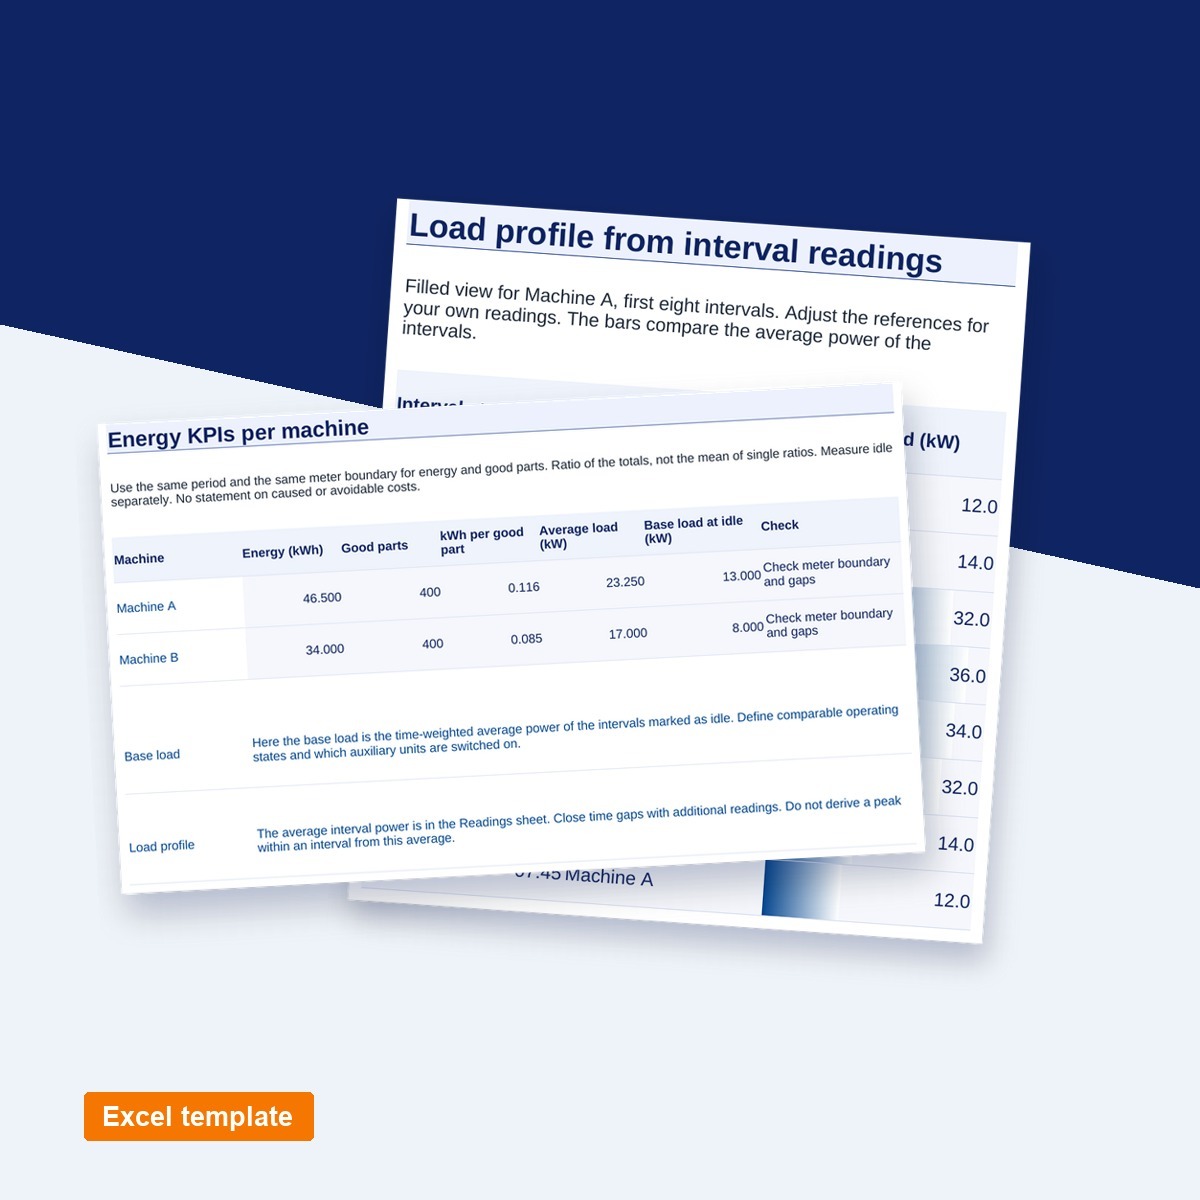
Energy KPIs per Machine
Calculate kWh per good part and idle load for each machine from your own meter readings.
- Meter log with readings, time intervals and good quantity
- kWh per good part and time-weighted idle base load per machine
- Load profile from interval values with data bars
Excel
Energy KPIs per Machine
- Meter log with readings, time intervals and good quantity
- kWh per good part and time-weighted idle base load per machine
- Load profile from interval values with data bars

Responsible since 2014 for the architecture of the cloud MES platform on Microsoft Azure, from machine connectivity to real-time data processing. B.Sc. in business informatics.
- Cloud-native MES Architecture
- Microsoft Azure
- Microservice Architecture
- OPC UA
Updated
All articles by Mark Kobbert