


Contents
What is process evaluation?
Process evaluation is the systematic scoring of a manufacturing process against defined criteria — specifications, benchmarks, targets or maturity levels — to determine whether it is good enough, and by how much. It is the judgement layer that sits on top of raw data and process analysis. Synonyms in common use: process assessment, process appraisal, Prozessbewertung.
The distinction that matters: process analysis asks what is happening; process evaluation asks how good what is happening actually is. Analysis produces data; evaluation produces a verdict. Both are necessary, and the verdict is often more generous than the data supports. That gap — between the evaluation reported in the management meeting and the evaluation the data would produce if left alone — is where most operational truth gets lost.
What is the difference between process analysis and process evaluation?
In practice, the two are inseparable — you cannot evaluate honestly without analysing first — but plants frequently try. They jump to a verdict based on averages, gut feel and the most recent shift, and skip the analytical work that would give the verdict a foundation. The result is an evaluation that is technically a number but functionally an opinion.
What are the main methods of process evaluation?
Four method families cover most of what plants actually use:
- Process capability analysis (Cp, Cpk, Pp, Ppk). The statistical workhorse. Compares process output distribution to specification limits. Short-term vs. long-term (Pp/Ppk) is the critical distinction most plants ignore.
- KPI benchmarking. Compares the process against internal or external reference points — sister plants, industry norms, historical best. Fast, intuitive, and dangerously prone to apples-to-oranges comparisons.
- Maturity models. Structured assessment against a staged framework (CMMI, Lean maturity, Industry 4.0 maturity indices). Produces a level score. Useful for transformation programmes, less useful for daily operations.
- Audit-based evaluation. Scored assessment against a checklist — IATF 16949, VDA 6.3, ISO 9001 process audits. Required for regulated industries; often disconnected from operational reality.
Every method has a characteristic failure mode. Capability indices get inflated by short data windows. Benchmarks drift toward favourable comparisons. Maturity models reward documentation over results. Audits score the system on the day of the audit. The honest evaluator uses at least two methods and notices when they disagree — because when they disagree, at least one of them is lying.
What do process capability indices actually mean?
The trap is Cp versus Cpk. Cp measures what the process could do if perfectly centred. Cpk measures what it actually does given its real centring. A process with Cp = 1.67 and Cpk = 0.8 looks capable on paper and is a defect factory in practice. Reporting Cp instead of Cpk is the oldest trick in the evaluation book, and it appears in many management reports.
Why do process evaluations systematically over-state performance?
This is the part nobody wants to write down. In many plants, the reported evaluation is more favourable than the evaluation the raw data would produce. The mechanisms are always the same:
- Selection bias in the data window. Capability calculated from "a representative week" that conveniently excluded the bad shifts.
- Exclusion of special-cause events. "That breakdown wasn't a normal process event, so we didn't count it." Every exclusion is a vote for the process looking better than it is.
- Rounding toward the target. Maturity scores of 2.7 reported as "Level 3." Cpk values of 1.29 reported as "around 1.33."
- Spec-limit creep. Specifications widened quietly to accommodate process reality, then capability recalculated against the new limits.
- Averaging across heterogeneous populations. Evaluating a process across three products with different tolerances produces an average that means nothing and looks fine.
- The Hawthorne effect. Processes behave better when they know they are being evaluated. Short assessment windows catch the best version of the process, not the normal one.
None of this is usually dishonest in intent. It is the cumulative drift of many small decisions made under organisational pressure to report a number that keeps everyone comfortable. The cure is not better morality; it is automatic, continuous measurement that does not bend to convenience. A capability index calculated in real time across every part produced tells a truth that weekly spot checks cannot.
How do you conduct an honest process evaluation?
- Define the evaluation question precisely. "Is the press capable" is not a question. "Is the press producing dimension X within specification at Cpk ≥ 1.33 across all three shifts and both material batches" is a question.
- Use the full population, not a sample. With automatic data capture, there is no reason to evaluate on samples any more. Use every part.
- Report Ppk alongside Cpk. Long-term performance against short-term capability. The gap between them reveals how well the process holds up over time.
- Segment before scoring. Evaluate each product, each shift, each material batch separately before aggregating. Averages destroy information.
- Cross-check with a second method. A Cpk of 1.5 and a defect rate of 2% do not coexist in an honest evaluation. If they appear together, one of them is wrong.
- Publish the evaluation method, not just the result. An evaluation you cannot reproduce is not an evaluation — it is an assertion.
FAQ
What is the difference between Cp and Pp?
Cp uses short-term variation (within a single batch or time window); Pp uses long-term variation (across all variation sources including setup, material, shift changes). Pp is almost always smaller than Cp. Reporting only Cp is the most common single distortion in capability evaluation.
Is Cpk 1.33 really the right target?
For serial production of non-critical characteristics, yes. For critical safety characteristics in automotive, 1.67 or 2.00 is required. For small-series production with few parts, classical Cpk is statistically unreliable and alternative methods (tolerance intervals) are more honest.
How often should processes be evaluated?
Statistical capability: continuously when automatic measurement allows it, otherwise at minimum monthly for serial production. Maturity and audit-based evaluation: annually, with interim progress reviews. The old model of "quarterly capability studies" belongs to the era before real-time measurement.
Can process evaluation be automated?
The calculation, yes — Cp, Cpk, Pp, Ppk, yield, defect rates are all deterministic functions of the underlying data. The interpretation remains human. A Cpk of 1.2 in one context is a crisis; in another it is acceptable. That judgement cannot be automated and should not be.
What's the relationship between process evaluation and OEE?
OEE is a specific evaluation method, focused on availability, performance and quality combined into a single score. Process evaluation is broader — it includes statistical capability, maturity, conformance to standards, and benchmarking. OEE tells you how much saleable output the process produces relative to its theoretical maximum; capability evaluation tells you how reliably it hits specification within that output.
Why do audit-based evaluations often contradict operational data?
Audits evaluate the documented process on the day of the audit. Operational data evaluates the actual process across all days. If the documented process is aspirational and the actual process is different, the two will disagree — and the operational data is almost always closer to reality. A process that passes an IATF audit with gaps in its real capability is a latent customer complaint waiting to happen.
How does SYMESTIC support process evaluation?
SYMESTIC captures per-part measurements, stop events, reason codes and process parameters automatically through Production Metrics and Process Data. The monthly capability report used to be a spreadsheet built on Friday from data pulled Thursday; today the same report is live, continuous and segmentable by product, shift and material batch. The shift that makes possible — from occasional evaluation to continuous evaluation — is what turns the verdict from opinion into evidence.
Related: OEE · MES · Process Analysis · Productivity Metrics · Statistical Process Control · Six Sigma · Production Stability · First-Pass Yield · Production Metrics · Process Data.
See process data that supports Cp and Cpk
In a live demo we show how process values are recorded at the machine and evaluated over time.
- Live OEE
- Downtime and reasons
- Connecting machines and ERP
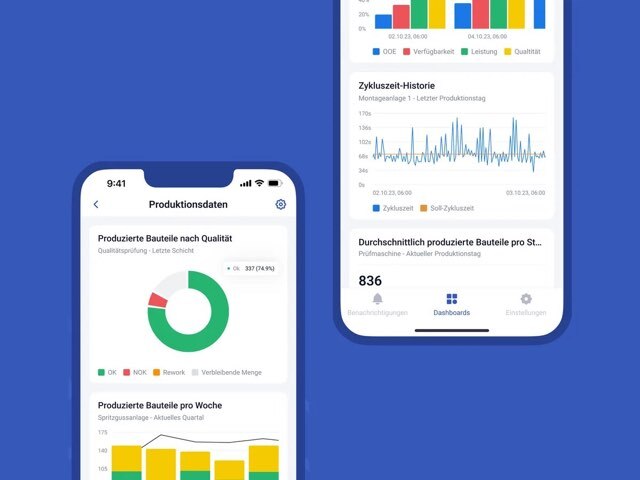
Spot deviations before scrap occurs
SYMESTIC checks process values continuously against your limits and alerts you while the part is still good.