Process control is the monitoring and regulation of manufacturing processes so that they stay within defined parameters and produce consistent output. The term sounds narrow but is used for three quite different disciplines: advanced process control (APC) inside continuous processes, statistical process control (SPC) for discrete quality management, and in-process monitoring — the real-time capture of process parameters from machines. A modern MES is almost always talking about the third, often in combination with SPC, and very rarely about APC in the classical sense.
This matters because the tooling, the audience and the expected result differ sharply between the three. A chemical engineer, a Six Sigma Black Belt and a production manager can all say "we need process control" in the same meeting and mean three different things. Sorting that out in the first ten minutes is worth more than any vendor comparison that follows.
The three things "process control" actually means
Type
What it regulates
Primary tooling
Typical industry
Advanced Process Control (APC)
Continuous physical variables (temperature, pressure, flow) via closed-loop regulation
DCS, PID controllers, model-predictive control
Chemical, refining, pulp & paper, power
Statistical Process Control (SPC)
Process stability & capability over time, using statistical rules
Control charts (X-bar/R, p, c), Cp/Cpk
Discrete manufacturing, automotive, medical
In-process monitoring
Live machine parameters (cycle values, pressures, positions, energy) per part or batch
MES, process data module, OPC UA capture
All discrete and batch production
APC lives inside the machine — it is a control-engineering discipline that existed long before MES and will continue to exist alongside it. SPC is a statistical method, historically paper-based, now almost always running inside a quality module or MES. In-process monitoring is the newest of the three and the one with the largest practical impact on discrete manufacturing in the last decade: for the first time, the actual process parameters that ran when a specific part was produced can be stored, correlated with reject events and retrieved years later for a customer complaint.
Process control vs. production control vs. quality control
Three adjacent terms that are routinely mixed up:
Figure: Three adjacent disciplines that a well-run plant connects.
Process control — keeps the process parameters inside their defined window (injection pressure, welding current, oven temperature).
Production control — keeps the order flow on track (dispatching, sequencing, reacting to disruptions). This is the classical MES execution layer.
Quality control — judges the output against specification (inspection, SPC, release decisions).
A well-run plant does all three and connects them. A poorly-run plant optimises one in isolation and is then surprised that the others fail.
Why in-process monitoring is the part MES buyers actually care about
For a discrete or batch manufacturer evaluating an MES, "process control" is almost always shorthand for in-process monitoring plus SPC — the ability to capture process parameters continuously, correlate them with part outcomes, and flag drift before it becomes scrap. The APC layer is already solved by the machine vendor; no MES replaces a PID loop. What the MES adds is three things the machine alone cannot provide:
Persistence across parts and batches. The PLC knows the current pressure. Only the MES remembers which pressure ran on part serial 482193 at 03:14 last Tuesday.
Correlation across machines. A quality escape is rarely caused by one machine alone. Correlating process data across upstream and downstream steps is how root causes actually get found.
Control limits. Process data shows control limits and Cp/Cpk for a process parameter.
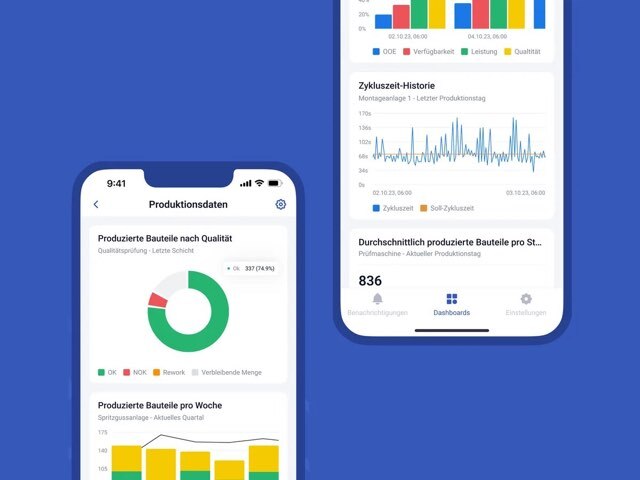
Concretely, this is what SYMESTIC's Process Data module does: it captures parameters via OPC UA or digital I/O, stores them against the production order and part, and makes them queryable alongside stop reasons, reject counts and OEE.
Common pitfalls
Pitfall
What goes wrong
Counter-measure
Capturing everything, analysing nothing
Terabytes of process data with no link to outcomes
Define the top 5 parameters per process first; expand later
SPC without context
Control charts exist but nobody reads them; out-of-control signals ignored
Wire SPC alerts into the shopfloor UI, not a separate report
No part-level traceability
Process data stored against time only — cannot answer "which parameters ran on this serial?"
Store parameters against order + part; integrate with traceability
Specification drift
Parameter limits set at machine commissioning and never revisited as process matures
Quarterly review of Cp/Cpk; tighten limits when capability allows
FAQ
Is process control the same as SPC? No. SPC is one specific method within process control — a statistical technique for judging whether a process is stable over time. Process control as an umbrella term also covers closed-loop regulation inside machines (APC) and continuous in-process monitoring via an MES. In most discrete-manufacturing discussions, "process control" used without qualification means in-process monitoring combined with SPC, which is also what a modern MES delivers.
Does an MES replace DCS or PLC-level control? No, and it shouldn't try. The control-engineering layer — PID loops, safety interlocks, real-time regulation — belongs inside the machine and runs at cycle times an MES cannot reach. What the MES adds sits one layer above: capturing the parameters the PLC is already using, storing them against the production order, correlating them with outcomes, and making them queryable for root-cause analysis and traceability.
Which process parameters should we capture first? Start with the parameters that operators already watch and that show up in reject discussions — typically five to ten per process step. Injection pressure and cycle time for moulding, welding current and duration for joining, oven temperature and belt speed for curing. Capturing everything the PLC exposes on day one produces volume without insight; capturing the parameters with a known quality link produces immediate return and creates the habit of looking at the data.
How does SYMESTIC support process control? Through the Process Data module, which captures parameters directly from the PLC via OPC UA or digital I/O, stores them against production order and part, and integrates with reject capture and OEE in one platform. The typical deployment pattern across the 15,000+ machines SYMESTIC has connected: start with OEE and stop-reason capture, add process data on the two or three most reject-sensitive parameters per process, and expand from there. Go-live is measured in days, not months.
Six Sigma Black Belt with more than 25 years in manufacturing, previously at Johnson Controls, Visteon, iTAC and Dürr. Author of the book “OEE: Eine Zahl, viele Lügen”.