
MES Software: Vendors, Features & Costs Compared 2026
MES software compared: vendors, functions per VDI 5600, costs (cloud vs. on-premise) and implementation. Honest market overview 2026.
Process quality is the degree to which a production process produces conforming output consistently, without drift, with predictable variation, and with enough margin against specification limits to absorb normal disturbances. It is not the same as product quality. Product quality describes what comes out of the process; process quality describes how reliably the process produces it. A factory can ship good parts while having poor process quality — it just happens by inspection and rework, at full cost of poor quality. And a factory can have excellent process quality that temporarily produces bad parts when inputs shift. The two dimensions are related but independent, and quality engineering exists largely to keep them distinct.
The cleanest framing comes from Avedis Donabedian's quality triad, originally developed for healthcare but widely adopted in manufacturing: structure (the resources, equipment, people and systems available), process (how those resources are used to transform inputs into outputs), and outcome (what the customer receives). Process quality is the middle layer — the one that is hardest to see from outside the factory and the one where most improvement leverage lives.
This is the single most important distinction on the topic, and it is the one most generic articles get wrong. High process quality requires two separate conditions, and both have to be true at the same time:
A process can be stable but incapable — it reliably produces bad parts. It can be capable but unstable — the average result meets spec but you cannot predict tomorrow's output. Only when both conditions hold is the process truly in good shape. Quality engineering has separate tools for each: control charts for stability, capability indices for capability. Confusing the two is the most common mistake on shopfloors that are trying to improve.
Once a process is stable, its capability is expressed through four closely related indices. They look similar, differ in subtle ways, and get confused constantly.
| Index | What it measures | Typical target |
|---|---|---|
| Cp | Potential capability (spread only — assumes process is perfectly centred) | ≥ 1.33 standard, ≥ 1.67 critical |
| Cpk | Actual capability (spread and centring — uses short-term variation) | ≥ 1.33 standard, ≥ 1.67 critical |
| Pp | Potential performance (like Cp but uses long-term variation) | ≥ 1.33 standard |
| Ppk | Actual performance (like Cpk but uses long-term variation) | ≥ 1.33 standard |
The practical rule of thumb: Cpk is the number you report to customers, Ppk is the number that tells you the truth over time. Cpk uses within-subgroup variation (short term) and tends to be optimistic. Ppk uses total variation (long term) and is what the customer actually experiences. A process with Cpk = 1.67 but Ppk = 1.10 is telling you that something shifts between subgroups — a shift change, a tool change, a material batch — and you haven't found it yet. In automotive PPAP practice the common requirement is Ppk ≥ 1.67 for the initial submission and Cpk ≥ 1.33 in ongoing production, depending on the customer.

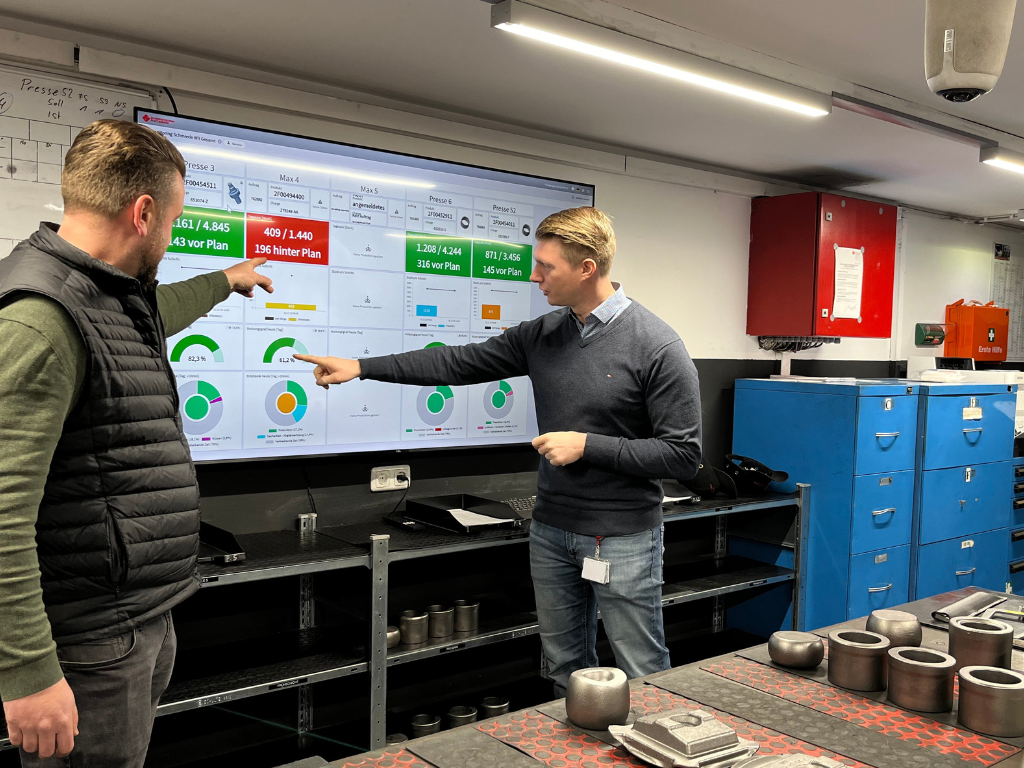
 Case Study
Process capability is often expressed as a sigma level, which translates directly into expected defects per million parts (DPPM or DPMO). The table below is the canonical reference every Six Sigma practitioner knows, with the 1.5-sigma shift Motorola introduced to account for long-term drift.
| Sigma level | DPMO (with 1.5σ shift) | Yield | Typical context |
|---|---|---|---|
| 2σ | 308,537 | 69.1 % | Uncontrolled process |
| 3σ | 66,807 | 93.3 % | Industry average for many processes |
| 4σ | 6,210 | 99.4 % | Competent manufacturing |
| 5σ | 233 | 99.977 % | Best-in-class automotive |
| 6σ | 3.4 | 99.9997 % | Aerospace, pharmaceuticals, semiconductor |
Moving from 3σ to 4σ is usually a bigger win financially than anything in the OEE availability or performance buckets — one sigma level is a 10× reduction in defect rate.
Walter Shewhart in 1924 and later W. Edwards Deming made a distinction that still defines modern quality thinking: variation has two sources, and confusing them is the single most expensive mistake in process management. Both sources are explained in the article on process variation.
Control charts exist to tell these two apart. Points inside the control limits with no trend = common cause, leave it alone, improve systemically. Points outside the control limits or showing non-random patterns = special cause, stop and investigate. In practice, operators are often pulled into "investigating" common-cause variation because management demands an explanation for every small fluctuation. That is where process quality collapses, not because the process is bad, but because the reaction to its normal variation is.
For decades, process quality was measured retrospectively: take samples, measure them offline, plot them on paper control charts, calculate Cpk at the end of the week. This is still how most mid-market plants operate. It works, sort of — but it turns process quality into a lagging indicator. By the time the Cpk report arrives on Monday, Friday's shift has already produced a full day of drifted output.
The current-generation answer is to capture process parameters continuously at the machine, run SPC rules against them live, and alert on special-cause signals in the moment they appear.
What is the difference between process quality and product quality?
Product quality describes how well the finished output meets specification and customer expectations. Process quality describes how consistently and capably the production process produces that output. High process quality almost always produces high product quality; the reverse is not true. See the related article on product quality for the customer-facing view.
Is high Cpk enough to declare a process "good"?
No. Cpk is only meaningful after stability has been established — usually by showing the process is in statistical control on a control chart for at least 20–30 subgroups. Calculating Cpk on an unstable process produces a number, but that number does not predict future behaviour. Ppk should always be compared with Cpk; a large gap between them indicates that something is shifting between subgroups and has not been identified.
What is considered good process quality in 2026?
It depends entirely on industry. Automotive PPAP work typically requires Ppk ≥ 1.67 for the initial submission and Cpk ≥ 1.33 in series production, depending on the customer. Medical devices and aerospace push higher. General discrete manufacturing benchmarks against Cpk ≥ 1.33. Anything below Cpk 1.0 is a process that produces some defects as a matter of design, not accident.
Do I need a full Six Sigma programme to improve process quality?
No. Six Sigma methodology (DMAIC, Black Belts, tollgate reviews) is valuable in large organisations with complex processes and a structured improvement culture. In a mid-market plant with ten production lines, the higher-leverage move is usually to instrument the process with real-time data capture first, and only then decide which DMAIC projects to start. Running DMAIC without live process data is possible but slow — you spend most of the Measure phase assembling data that should have been captured automatically.
What does SYMESTIC do for process quality specifically?
Three things, all delivered on the same platform. First, continuous capture of process parameters (temperature, pressure, cycle time, parameter values) at the machine via OPC UA or digital I/O. Second, capture of reject events and alarm signals at the PLC level, mapped to the production order. Third, process stability monitoring with control limits and Cp/Cpk per process parameter. The range SYMESTIC cites for scrap reduction is 5–15 % — not because statistics changed, but because the time between drift and detection collapsed.
Related: Product Quality · Statistical Process Control · Cp/Cpk · Six Sigma · Production Defect · Process Data Module
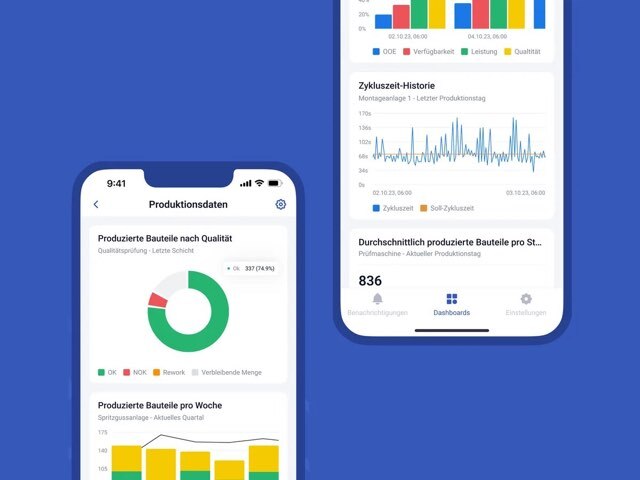
Scrap isn't made at inspection. It's made minutes earlier at the machine.
Intervene while the part is still good
SYMESTIC continuously checks process values such as temperature and pressure against your limits and alerts you on deviation.