


Contents
What are scrap costs?
Scrap costs are the full financial impact of parts that cannot be shipped and cannot be reworked — they leave the process as loss. In the OEE framework this is the hard end of the Quality factor, distinct from rework, which describes parts that are recovered. Synonyms in common use: reject cost, defective-part cost, Ausschusskosten.
The definition sounds simple, and every cost-accounting textbook treats it that way — number of scrapped parts multiplied by standard cost. On real shop floors, that calculation rarely comes close to the truth. The problem is not the arithmetic; it is that neither side of the multiplication is measured accurately.
How are scrap costs calculated?
The working formula, with all components counted honestly:
Scrap Cost = Material + Processing Cost to Point of Scrap + Disposal + Replacement Run + Downstream Impact
Each term deserves attention. Material is the raw input consumed in the scrapped part — usually the easiest to measure. Processing cost is every labour, machine and overhead hour consumed up to the moment the part was declared unrecoverable; a part scrapped at the final inspection has absorbed the full process, not just the station that detected the defect. Disposal covers handling, segregation, documentation and — increasingly — take-back and recycling costs. Replacement run is the additional line time required to produce the missing good part, including setup if it happens in a separate batch. Downstream impact covers late-shipment penalties and customer-line disruptions caused by missing volume.
The full-cost calculation is typically well above the standard-cost figure that most plants use.
What does the under-counting actually look like?
The one that surprises every plant is in-line auto-ejects. Modern machines eject bad parts automatically — a vision system sees a flaw and the part drops into a reject chute. No operator touches it, no one logs it. If the machine signal is not captured, that scrap simply does not exist in the data. Once the machine signal is captured, honest counting often shows noticeably more scrap than the operator reports, and nobody was lying: the data channel had never existed.
What do realistic scrap rates look like?
The column that matters is the last one. A plant reporting 1% scrap on paper is almost always at 2–4% in reality. This is not a criticism of the teams on the floor; it is a property of manual measurement under production pressure.
How do you actually measure scrap without guessing?
This is the unglamorous part of scrap reduction, and the step most plants want to skip. You cannot reduce what you do not measure, and in scrap the measurement problem is harder than in downtime or performance — because a bad part often looks, from the outside, identical to a good one until someone classifies it. The practical sequence:
- Capture good count and total count separately at source. Machine signals, not operator tallies. Good parts pass the final inspection station; total parts pass the first station. The difference is scrap — reliably, in real time, whether anyone writes it down or not.
- Log every eject event. Vision-system rejects, weight-check rejects, dimension-check rejects — each needs a signal line and a reason code. This is a brownfield problem: most existing machines have the signals available; they just were never wired into a data-capture system.
- Separate start-up scrap from running scrap. Two different root causes, two different corrective actions. Plants that lump them together optimise neither.
- Classify at source. A defect reason logged ten hours later is a guess. A reason logged when the operator is still at the station is data. This is where MDE/BDE discipline either pays off or collapses.
None of this requires a Six Sigma black belt or a predictive-analytics platform. It requires the data channels to exist. Once they do, reduction follows almost automatically — because the reasons become visible in a Pareto, and three reasons cover most of the problem.
What actually reduces scrap costs?
In the order that works in practice: measurement first, Pareto second, process fix third, technology last. The temptation is always to reverse this — buy a vision system, install SPC software, implement predictive maintenance — on top of a measurement base that misses 30% of the problem. That produces expensive disappointment. When the measurement is honest, the top three defect reasons almost always point to one or two concrete process weaknesses: an unstable parameter, a worn tool, a material supplier variation. Fix those, and the scrap rate drops faster than any workshop plan predicted.
FAQ
What's the difference between scrap and rework?
Scrap is unrecoverable loss. Rework is defective parts that get recovered through additional operations. Both are Quality losses in OEE; the financial treatment differs because scrap destroys the full invested cost while rework recovers part of it.
How is scrap cost related to OEE?
Directly. Scrapped parts count as Quality losses in OEE — produced but not saleable.
Should start-up scrap be counted the same as running scrap?
Count it, but separately. The root causes are completely different — start-up scrap is about warm-up, parameter convergence and first-off inspection. Running scrap is about process stability during production. Combining them makes both problems invisible.
What's a realistic scrap reduction target in the first year?
For plants moving from manual counting to automatic capture, 25–40% reduction in measured scrap within 12 months is common — but most of that comes from fixing the top two or three defect reasons, not blanket improvement. The first Pareto usually points to something obvious that nobody had data to prove.
How is scrap cost affected by the scrap-value recovery (recycling)?
Recovery reduces net scrap cost but rarely meaningfully. Recycled material typically returns 10–30% of its original value. The replacement-run cost, the lost capacity and the disposal handling usually dwarf the recycling credit. Do not let the recycling revenue mask the underlying process loss.
Why do plants resist measuring scrap automatically?
Because the number goes up. Reported scrap usually rises after automatic capture, and the first reaction is often "the new system is wrong". It isn't; the old measurement was. Plants that understand this see it as the starting point for real improvement. Plants that don't roll the system back.
How does SYMESTIC handle scrap capture on existing machines?
Via digital-I/O gateways, OPC UA and MQTT connections that read good-count, total-count and eject signals directly from the machine — no PLC modification, no production interruption. Reason codes are captured at source through Production Metrics shopfloor clients, which means scrap classification happens while the operator is still at the station. For plants starting from manual tracking, the first week of honest data is typically the most revealing week of the year.
Related: OEE · MES · Rework · Quality Losses · Production Stability · Statistical Process Control · Six Sigma · Machine Data Collection · Production Metrics · Process Data.
Calculate the full cost of your scrap
In a free 30-minute call we add material and machine time to your scrap and calculate the annual cost. No software demo.
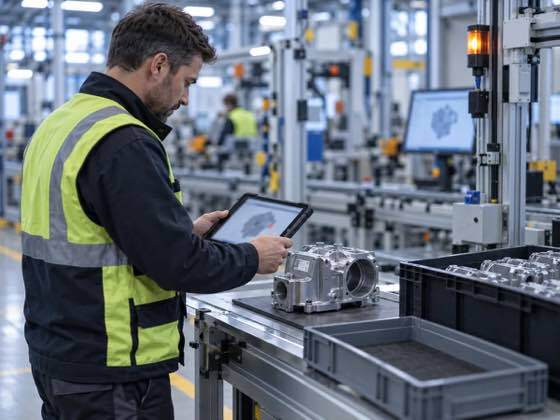
Every defect recorded, every defect costed
Scan the part, choose OK or NOK, tap the defect location. SYMESTIC shows which defect occurs how often and what it costs.