




Contents
What is maintenance planning?
Maintenance planning is the structured definition, scheduling and control of all activities required to keep production assets available, reliable and safe. It translates equipment criticality, failure history, manufacturer recommendations and condition data into a concrete calendar of inspections, preventive tasks, overhauls and spare-part reservations. In German: Instandhaltungsplanung. It is the tactical layer between the maintenance strategy (reliability policy) and the work-order execution handled by a CMMS or MES maintenance module.
Maintenance planning is the single biggest lever on availability — the first factor of OEE. Unplanned downtime is typically considerably more expensive per hour than planned downtime. Moving one hour from unplanned to planned is pure margin recovery.
Maintenance planning vs. maintenance scheduling vs. maintenance strategy
These three terms sit on top of each other in every serious RFP and get swapped almost every meeting. The distinction matters because the decision right and the required data are different at each layer.
Strategy decides whether a bearing is run-to-failure or condition-monitored. Planning decides the scope and frequency of the inspection. Scheduling decides that technician Müller replaces it on Thursday during the planned 90-minute window. Skip any of the three and the other two collapse into firefighting.
Which maintenance strategies feed the plan?
A maintenance plan is only as good as the strategy behind each asset. Four strategies dominate, and almost every real plant runs all four in parallel on different equipment.
- Reactive (run-to-failure): deliberate for low-criticality, cheap-to-replace assets. Dangerous when applied by default.
- Preventive (time or cycle based): fixed intervals from OEM data or experience. Simple, but over-maintains stable assets and under-maintains stressed ones.
- Condition-based (CBM): triggered by measured parameters — vibration, temperature, current draw, cycle count, oil analysis. Requires sensors and thresholds.
- Predictive (PdM): model-based forecasting of remaining useful life from streamed condition data, often with ML on top of the MES/historian. Highest upside, highest data requirement.
The correct strategy per asset is an economic decision, not a technology preference. Assign it from a criticality matrix (failure probability × production impact × safety/quality risk), not from whatever the last conference talk recommended.
How does MES data change maintenance planning?
Traditional maintenance planning lives in a CMMS fed by manual entries — hour-meter readings, operator tickets, post-mortem downtime logs. The plan is only as good as the discipline of the person updating the sheet. With an MES streaming live machine states, the picture changes in three ways. Actual running hours replace estimated ones, so preventive intervals trigger on real wear instead of calendar assumptions. Stop-reason codes captured at the source reveal failure patterns that no paper log catches — micro-stops under 3 minutes, repeat alarms, creeping cycle-time drift. And condition signals available on OPC UA or digital I/O (motor current, chamber temperature, cycle pressure) feed CBM thresholds without a separate sensor project.
The practical effect: the maintenance plan stops being an annual PDF and becomes a living artifact that self-corrects against the reality captured on the shop floor every shift.
Which KPIs prove the plan is working?
Measure the plan with a compact set, reviewed monthly at the works-council level, not a 40-metric dashboard nobody opens.
- MTBF (mean time between failures) — the reliability trend per asset class.
- MTTR (mean time to repair) — how fast the organisation recovers when things break.
- Planned maintenance ratio (PMR): planned work-order hours ÷ total maintenance hours. World-class > 80%. Below 50% means the team is trapped in reactive mode.
- Schedule compliance: percentage of planned tasks completed in the planned week. Below 85% and the plan is fiction.
- Maintenance cost per unit produced — the economic truth test.
- Availability from OEE — the downstream effect everyone actually cares about.
Track these per line, not per plant. Aggregate numbers hide the bottleneck where 80% of the pain lives.
What this looks like in the SYMESTIC deployment pattern
At Meleghy Automotive across four plants, OEE capture on press and joining lines drove a 10% downtime reduction. At Klocke, all packaging lines went live within three weeks without PLC intervention. For authoritative frameworks, see the VDI 2890 guideline on planned maintenance and ISO 22400 manufacturing KPIs including availability and MTBF definitions.
FAQ
What is maintenance planning in manufacturing?
Maintenance planning is the structured definition of what maintenance work needs to be done on each production asset, at what frequency and with what resources. It translates the maintenance strategy (reactive, preventive, condition-based, predictive) into concrete task lists, spare-part forecasts and a rolling 12-month plan. Scheduling then assigns those tasks to specific days and technicians.
Maintenance planning vs. preventive maintenance — are they the same?
No. Preventive maintenance is one of four strategies that can feed a plan; maintenance planning is the discipline of building and maintaining the plan itself. A plan can contain preventive, condition-based, predictive and deliberate reactive elements in parallel — different strategies for different assets based on criticality and cost of failure.
Why do maintenance plans fail in practice?
Three reasons dominate. First, intervals copied from OEM recommendations without calibration against the plant's actual duty cycle. Second, no feedback loop from shop-floor failure data back into the plan — it stays a static PDF. Third, schedule compliance tracked as a vanity metric while planned maintenance ratio stays below 60%, meaning the team is drowning in reactive work and the plan is fiction. Fix the feedback loop first.
How long does it take to build a real maintenance plan?
For a single plant with connected machines, a usable first-pass plan takes 6–10 weeks: two weeks of asset criticality ranking, two to three weeks of failure-history analysis from MES and CMMS data, two weeks of task and interval definition with maintenance leads, and one to three weeks of spare-part alignment. A fully tuned plan needs 12 months of data to converge.
Do I need a CMMS or is MES enough?
MES and CMMS solve adjacent problems. MES captures what happened on the machine — stops, alarms, cycles, condition signals. CMMS manages the work — work orders, spare parts, technician hours, compliance records. A small plant can run maintenance from the MES alone if the team is disciplined. Above roughly 50 assets or in regulated environments, a dedicated CMMS integrated with the MES is the right architecture.
What role does predictive maintenance play?
Predictive maintenance is the top layer, not the foundation. It depends on a solid preventive and condition-based plan already in place, plus clean streaming data from the MES. Starting with PdM before the basics are in order delivers impressive dashboards and no availability gain. The sequence is reactive discipline → preventive calibration → condition-based triggers → predictive models.
How does SYMESTIC support maintenance planning?
Through live stop-reason capture via alarms, condition signals via process data, availability and MTBF/MTTR KPIs via production KPIs, and integration with existing CMMS and ERP systems. Machine connection via OPC UA or digital I/O gateways in days, not months — at Klocke, all packaging lines went live within three weeks without PLC intervention.
Related: MES · OEE · Availability · MTBF · MTTR · Predictive Maintenance · TPM · Alarms · Process Data · Maintenance Manager.

See maintenance data next to machine stops
In a live demo we show how stops and alarms are recorded per machine. Your maintenance planning can start from this data.
- Live OEE
- Downtime and reasons
- Connecting machines and ERP

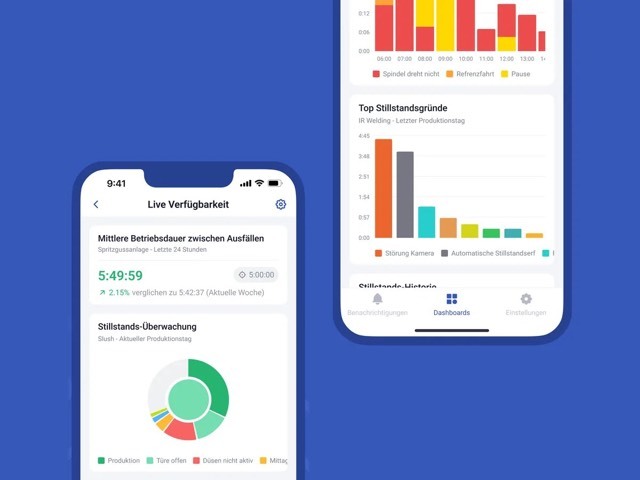
Know why the line stopped, not just for how long
SYMESTIC detects every stop at the machine, and the operator picks the reason. Meleghy Automotive cut downtime by 10% with SYMESTIC.
−10%downtime
Automotive supplier cut downtime by 10%
Meleghy Automotive also raised output by 7%. Started on one press line, SYMESTIC ran in all four plants six months later.