Machine availability is the percentage of planned production time during which a machine is actually able to run. It answers a single, blunt question: when the line was supposed to be working, how much of that time was it working? Everything else — performance losses, quality losses, changeover philosophy — is a separate discussion. Availability is the first of the three OEE factors and usually the one that exposes the biggest gap between what a plant believes and what is really happening.
If availability has never been measured automatically, the current number is likely wrong, and not by a little. Not occasionally — systematically. It is one of the most over-reported metrics in manufacturing.
The formula — simple arithmetic, tricky definitions
Availability (%) = Run Time ÷ Planned Production Time × 100
Where:
Planned Production Time = Scheduled Time − Planned Stops (breaks, no orders, scheduled maintenance, shift handovers if defined that way).
Run Time = Planned Production Time − Unplanned Stops (breakdowns, material shortages, minor stops, setup overruns).
The arithmetic is trivial. The arguments happen over what belongs in each bucket. Is a 12-minute tool change "planned" or "unplanned"? Does a 40-second micro-stop count? If the operator is waiting for material, is that the machine's availability loss or the logistics department's problem? The formula gives one answer; the politics inside a plant give seven.
Figure: How run time follows from scheduled time.
Realistic availability benchmarks by process
A 70 % availability means completely different things in different industries. Use the numbers below as a sanity check against your own, not as targets.
Process
Typical
Good
World-class
Injection moulding
75–82 %
85–88 %
92 %+
Automotive stamping
65–75 %
80–85 %
90 %
CNC machining
60–72 %
80 %
85 %+
Packaging (F&B, pharma)
65–78 %
85 %
92 %
Automated assembly
70–80 %
85–90 %
93 %+
Metal forming / forging
55–70 %
78–82 %
88 %
Availability vs. OEE — the distinction that gets forgotten
Availability is one of three OEE factors, not a synonym for OEE. The other two are performance and quality. A machine can sit at 95 % availability while running 20 % below speed and producing 8 % scrap — in which case the headline availability number is misleading. OEE multiplies the three factors:
OEE = Availability × Performance × Quality
The practical consequence: if your plant only tracks availability, you are optimising one-third of the picture. A line that improved availability from 72 % to 85 % while performance slid from 95 % to 82 % has not improved at all — it has just moved the loss from one column to the next.
Why reported availability is almost always wrong
Four systematic biases inflate self-reported availability:
1. Micro-stops disappear. Any stop under about two minutes falls below the threshold operators manually log. Multiply twenty micro-stops per shift by 90 seconds each and you have 30 minutes of invisible downtime — roughly 6 % of an eight-hour shift, gone. A reported "95 % availability" can turn into a much lower honest figure the week an MES goes live, without anything on the shopfloor having changed.
2. Changeovers get renamed. Some plants define changeover as planned stops and remove them from the denominator. Others call them unplanned. The same line can show 85 % or 72 % availability depending on which definition the controller preferred that month. This is not measurement; this is creative accounting.
3. The operator reason code is "unknown". When someone has to pick a stop reason from a paper list or a touchscreen after the fact, the default choice is the least controversial. "Material" when it was a breakdown. "Technical" when it was a skill gap. Without automated tagging from PLC alarms, the Pareto of stop reasons is fiction.
4. Scheduled time gets stretched. If a line ran overtime on Friday to recover from a Wednesday breakdown, some plants book the overtime against Friday's planned production time — which makes Wednesday's availability look better because the gap was "made up". Mathematically legal, operationally dishonest.
How to raise availability — what actually works
Three levers, in the order they should be pulled:
Attack micro-stops first. The long tail of sub-5-minute stops almost always dominates total downtime. A Pareto of stop reasons from one week of automatic capture usually shows that fixing the top three causes recovers 10–15 percentage points of availability. This is the single highest-ROI intervention in any availability programme.
SMED on changeovers. Structured changeover reduction routinely cuts setup time by 50–90 %. Every minute saved is a minute of run time gained.
TPM for breakdown reduction. Total Productive Maintenance — autonomous maintenance routines, condition monitoring, planned interventions — attacks the big-stop end of the distribution. Slower to show results than micro-stop work, but it is what moves availability from "good" to "world-class" in the final 5–8 percentage points.
The Meleghy Automotive rollout across four plants illustrates the pattern: 10 % reduction in stop time and 7 % throughput improvement — in six months, with no new equipment, driven by making the losses visible and working the Pareto systematically.
FAQ
What is a "good" machine availability number? There is no universal answer. World-class is usually considered 90 %+ for continuous processes, 85 %+ for discrete manufacturing. Anything above 95 % in a non-continuous process usually means the definition is wrong, not that the plant is a unicorn.
Does planned maintenance count against availability? By the standard OEE convention, no — it sits outside planned production time. Some plants include it anyway to force maintenance discipline into the headline KPI. Both are defensible; inconsistency between sites is not.
How fast should availability be measured? Sub-second state capture at the machine, aggregated to a minute or shift level for reporting. Hourly or shift-end manual entries miss 60–80 % of the real loss and make the number nearly useless for improvement work.
Is machine availability the same as uptime? Close but not identical. Uptime is a raw clock number — how long the machine was powered on and running. Availability is normalised against planned production time, so it is a percentage. An always-on machine can have high uptime and poor availability if it sat idle during planned shifts.
What software do I need to measure it automatically? An MES or OEE platform reading machine states from the PLC — via OPC UA on modern controls, digital I/O gateways on brownfield machines. SYMESTIC's Production Metrics captures availability as a day-one capability; typical rollout time is hours per machine, not weeks.
Why do availability numbers drop after we install an MES? Because for the first time they are correct. The pre-MES number was built on operator estimates and missing micro-stops. The post-MES number is lower and true. This is not a regression — it is the moment the measurement finally starts meaning something.
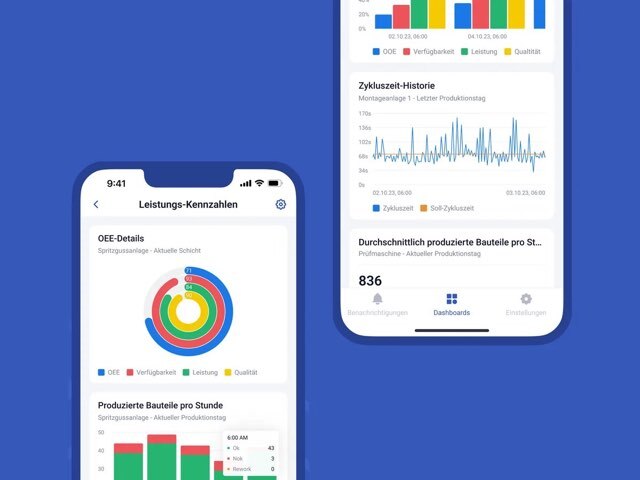
In a free live demo, a product expert walks you through the running platform and shows what OEE, downtime and the connection of your machines and ERP look like in practice.







 Case Study
