


Contents
Kaizen (改善) is a Japanese philosophy meaning "change for the better." In manufacturing, it translates to a daily practice of small, incremental improvements driven by every employee — from the shop floor operator to the plant manager. Unlike project-based methods like Six Sigma, Kaizen is not a tool you deploy — it is a way of working. Its power comes from frequency: 100 improvements of 0.1 % beat one restructuring of 10 %. But Kaizen without data is just opinion. An MES with real-time OEE dashboards turns Kaizen from philosophy into measurable system.
Table of contents
- What does Kaizen mean?
- What are the 5 core principles of Kaizen?
- Kaizen event vs. daily Kaizen — what is the difference?
- What is a Gemba walk?
- Why does Kaizen need real-time data?
- Kaizen vs. Six Sigma vs. Lean — how do they relate?
- What are the limits of Kaizen?
- FAQ
What does Kaizen mean?
Kaizen (改善) is composed of two Japanese characters: kai (change) and zen (good). The term was formalized by Masaaki Imai in his 1986 book Kaizen: The Key to Japan's Competitive Success and describes a culture of continuous, incremental improvement involving every person in an organization.
Kaizen draws on Japanese post-war quality-control practice and became the philosophical foundation of the Toyota Production System (TPS). While Toyota made it famous, the philosophy is now applied across manufacturing, healthcare, logistics, and service industries worldwide.
The core idea is deceptively simple: no process is ever perfect. Every day, there is something that can be improved — even if only by a small amount. What makes Kaizen different from other improvement methodologies is that it does not wait for a project, a budget, or a consultant. It happens today, at the workplace, by the people who do the work.
What are the 5 core principles of Kaizen?
| Principle | What it means | In manufacturing practice |
|---|---|---|
| 1. Know your customer | Improvement is only real if it creates value from the customer's perspective | In production, "customer" includes the next process step — every handoff is a customer relationship |
| 2. Let it flow | Eliminate waste (muda), unevenness (mura), and overburden (muri) to create smooth flow | Reduce WIP, eliminate bottlenecks, standardize changeovers |
| 3. Go to Gemba | Improvements come from the real place of work, not the meeting room | Managers walk the shop floor daily; problems are observed, not just reported |
| 4. Empower people | Every employee is a source of improvement ideas — not just engineers or managers | Operators submit ideas, teams solve problems, leadership enables and recognizes |
| 5. Be transparent | Make performance visible so everyone can see the current state and the gap to the target | Real-time OEE dashboards on the shop floor, visual management boards, Andon systems |
These five principles are not sequential steps — they are simultaneous operating modes. A Kaizen culture exists when all five are active at the same time.
Kaizen event vs. daily Kaizen — what is the difference?
The term "Kaizen" is used for two distinct activities that serve different purposes. Understanding the difference is critical for implementation.
| Dimension | Kaizen event (Kaizen Blitz) | Daily Kaizen |
|---|---|---|
| Duration | 3–5 days, dedicated workshop | 15 minutes per shift, every day |
| Scope | One specific problem or area | Any improvement, any size |
| Team | Cross-functional, 5–8 people | Shift team, individual operators |
| Output | Implemented change + new standard | Small adjustment, idea submitted |
| Data need | High — baseline + post-event measurement | Medium — visible KPIs on the shop floor |
| Frequency | Monthly or quarterly | Every shift, every day |
| Risk | One-off project that fades without follow-up | Too small to notice if not tracked |
The strongest Kaizen cultures use both. Daily Kaizen creates the habit. Events solve the hard problems. Neither works without the other.
What is a Gemba walk?
Gemba (現場) means "the real place" — in manufacturing, it is the shop floor. A Gemba walk is a structured visit by a manager or leader to the production floor, not to inspect, but to observe, ask questions, and understand the actual state of work.
A Gemba walk follows three rules: go see (don't rely on reports), ask why (don't make assumptions), and show respect (don't blame). It is the opposite of management-by-spreadsheet — and it is the mechanism through which leaders identify improvement opportunities that never appear in dashboards or meeting minutes.
When combined with real-time OEE data displayed on shopfloor management boards, the Gemba walk becomes dramatically more effective: the leader sees both the physical reality and the data reality simultaneously. Discrepancies between the two are where the best Kaizen ideas hide.
Why does Kaizen need real-time data?
Kaizen's original form at Toyota relied on paper kanban boards, visual signals, and manual observation. That worked in the 1960s. In modern manufacturing — with higher speeds, more variants, and tighter margins — Kaizen without data is guesswork.
| Kaizen activity | Without MES | With MES |
|---|---|---|
| Daily standup: "What was our biggest loss yesterday?" | Shift leader recalls from memory | Pareto chart of downtime reasons on the screen |
| Kaizen event: "Did our changeover time improve?" | Stopwatch before, stopwatch after, hope it's representative | Automatic before/after comparison across 30 changeovers |
| Gemba walk: "Is line 4 running at target speed?" | "It looks okay" — no one checks cycle time deviation | Real-time performance factor visible on dashboard: 87 % of target |
| Sustaining gains: "Is the new standard holding?" | Manual audit once a month | Alert on defined conditions |

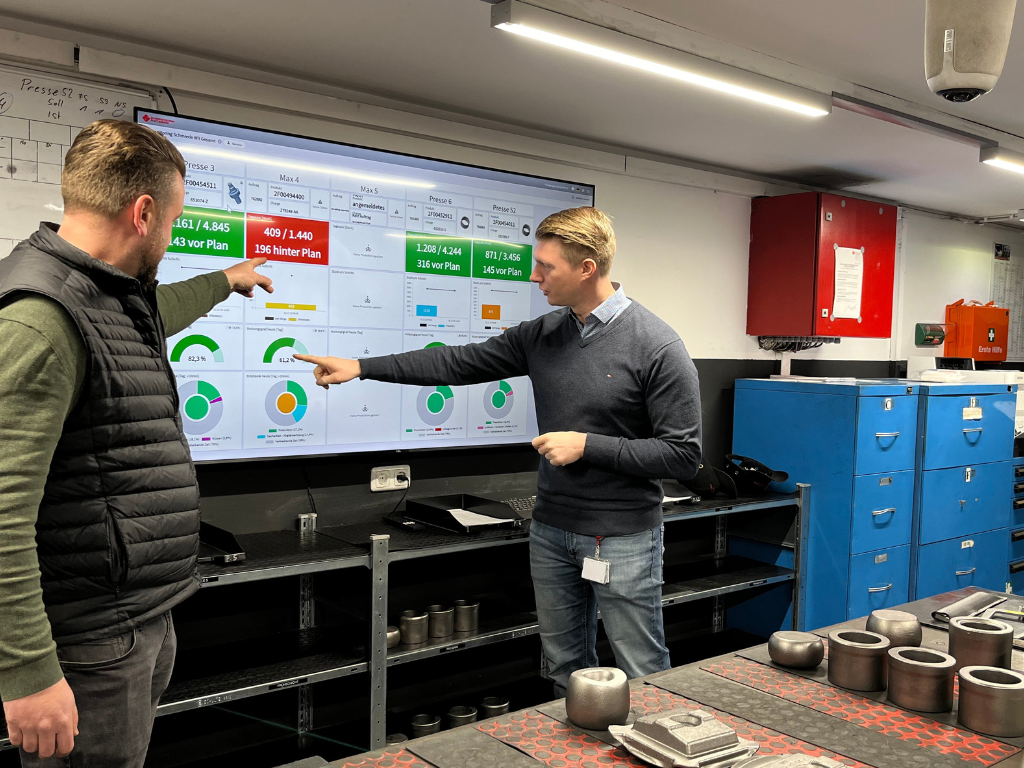
How Schmiedetechnik Plettenberg improves press performance with data
- Real-time OEE at every press
- Downtime reasons documented end to end
- Shift handovers backed by hard data
- Fast response to disruptions & bottlenecks
 Case Study
Kaizen vs. Six Sigma vs. Lean — how do they relate?
| Dimension | Kaizen | Six Sigma | Lean |
|---|---|---|---|
| Core idea | Every day, everyone improves | Reduce process variation statistically | Eliminate waste, create flow |
| Approach | Bottom-up, incremental | Expert-driven, data-intensive | System-level, value-stream-focused |
| Speed | Immediate - implement today | Weeks to months per DMAIC cycle | Varies — from quick wins to major redesign |
| Who drives it | Everyone | Certified Belts (Green, Black) | Cross-functional teams |
| Best for | Building culture, daily engagement | Complex quality problems, yield losses | Systemic waste, lead time reduction |
| Relationship | The daily habit | A specialist tool within CI | The system-level framework |
These are not alternatives — they are layers. Lean provides the system view. Kaizen provides the daily habit. Six Sigma solves the hard statistical problems. Together, they form the toolkit of Operational Excellence.
What are the limits of Kaizen?
Kaizen is powerful, but it is not a universal solution. Understanding its boundaries prevents disillusionment.
| Limitation | Why it matters | What to do instead |
|---|---|---|
| Not suited for breakthrough innovation | Incremental improvement cannot invent a new product or business model | Combine Kaizen (optimize existing) with dedicated innovation processes |
| Requires cultural commitment | Without leadership support, Kaizen degrades into a suggestion box nobody reads | 24-hour response to ideas, visible leadership on the Gemba |
| Hard to sustain under pressure | When deadlines tighten, "improvement time" is the first thing cut | Protect 15 min/day as non-negotiable. Make it a habit, not a project. |
| Invisible without data | Small improvements are hard to see without measurement — teams lose motivation | Use an MES to make every 0.5 % OEE gain visible and celebrated |
FAQ
What does Kaizen mean?
Kaizen (改善) is a Japanese word meaning "change for the better." In business context, it describes a philosophy of continuous, incremental improvement involving every employee. It was formalized by Masaaki Imai in 1986 and is the philosophical foundation of the Toyota Production System.
What is the difference between Kaizen and CIP?
Kaizen is the philosophy — the belief that everything can be improved, every day, by everyone. CIP (Continuous Improvement Process) is the structured operationalization: defined cycles (PDCA), tools, measurement, and governance. Kaizen is the mindset; CIP is the management system that implements it.
What is a Kaizen event?
A Kaizen event (also called Kaizen Blitz or Kaizen Workshop) is a focused 3–5 day workshop where a cross-functional team tackles one specific problem. It includes problem analysis, root cause identification, solution implementation, and verification — all within the workshop week.
How does Kaizen relate to Lean manufacturing?
Lean is the system-level framework for eliminating waste and creating flow. Kaizen is the daily practice that makes Lean sustainable. Without Kaizen, Lean becomes a one-time project. Without Lean, Kaizen lacks strategic direction.
How does an MES support Kaizen?
An MES provides the data foundation for every Kaizen cycle: real-time OEE, automatic downtime detection with the reason selected at the workstation, and before/after comparisons. It makes the "Check" step objective and the "Act" step evidence-based.
The bottom line: Kaizen is not a methodology to be "rolled out." It is a daily habit that becomes the operating system of a production facility. The habit forms when people see the result of their improvement — the next day, on the dashboard, in the numbers. Start with visibility. The culture follows the data. A live demo shows what that visibility looks like on real machine data.
→ CIP: Continuous Improvement Process · → OEE Explained · → What is an MES? · → Six Sigma · → Lean Production · → Shopfloor Management · → Operational Excellence
One machine. Four weeks. Your criteria.
Give your next kaizen event live data
In a proof of value we connect one of your machines for four weeks, so the next improvement starts from recorded stops and output.
- Connect one machine
- Measure live for four weeks
- Check the result against your criteria