




Contents
What is operating time?
Operating time is the net duration during which a machine, line or system is actively producing output. It is not the time the machine is powered on, scheduled or theoretically available.
It is closely tied to the availability factor of OEE (which subtracts breakdowns and changeovers) and, once micro-stops and idling are taken out as well, to the performance factor. It serves as the divisor in the hourly machine rate, and is one of the most frequently overstated numbers on production dashboards.
The honest version of this metric tends to be below the reported one. The reason is not cheating. Short stops, unreported setup overruns and quiet idling fall below the threshold that operators manually log. When a plant switches on automatic capture, the number drops and the real improvement work can finally begin.
Operating time vs. the terms it gets confused with
Five closely related time concepts show up in every manufacturing conversation. Mixing them up is the most common reason production and controlling never agree on the same number.
Operating time sits in the middle of this hierarchy. It is tighter than running time, because idling does not count. It is also different from productive time, which counts only output that passed quality. Operating time is the raw production duration, independent of yield.
The formula
Operating Time = Planned Production Time − (Unplanned Downtime + Changeover Time + Micro-Stops + Idling)
And the ratio used in OEE and reporting:
Operating Time Rate (%) = Operating Time ÷ Planned Production Time × 100
In the Six Big Losses logic, breakdowns and changeovers are availability losses, while micro-stops, idling and reduced speed are performance losses. The formula above is stricter than the availability time of OEE on purpose. It takes out both groups, so the result is the time in which the machine was actually producing.
A plant that needs the OEE availability figure subtracts only breakdowns and changeovers. Whichever convention a plant uses, it has to be fixed once and applied the same way at every site.
Worked example (assumed values). A line is scheduled 480 minutes per shift with 30 minutes of planned breaks, giving 450 minutes of planned production time. Unplanned breakdowns account for 45 minutes, one changeover for 18 minutes, micro-stops for 18 minutes and idling for 10 minutes. Operating time is 450 − 91 = 359 minutes, an operating time rate of 79.8 percent.
A manual log that records only the breakdowns and the changeover shows 450 − 63 = 387 minutes and 86.0 percent. The 28-minute gap is the micro-stops and the idling, which fall below the manual logging threshold. What really drives throughput is covered under production speed.
Where the reported number goes wrong
Four systematic biases inflate self-reported operating time.
1. Micro-stops disappear. Any stop below the threshold a plant has set for manual logging goes unrecorded. The operator fixes it and moves on. Twenty events per shift at 90 seconds each is half an hour of invisible downtime.
2. Setup overruns get reclassified. The plan says 12 minutes for a changeover; reality is 18. The extra 6 minutes often get booked under the prior order or under no category at all.
3. Idling counts as running. A machine powered on with no parts moving is often recorded as running, because the light is still on. Strict operating time capture only counts cycles where output is actually produced.
4. The end-of-shift round-up. When manual logs are filled in at shift end, the numbers get smoothed. Human memory favors the clean story over the messy truth.
Realistic operating time rates by process
There is no single realistic figure. The rate depends on the process type, on how many changeovers a shift needs and on which losses the plant subtracts, so a value is only comparable between machines of the same process that follow the same definition. Compare a line with its own baseline before comparing plants.
Why operating time matters for costing
Operating time is also the divisor in the hourly machine rate calculation. If the divisor is inflated by 20 percent, the hourly rate is understated by 20 percent.
Every product cost computed against that rate is wrong, and every make-or-buy decision based on that cost is biased toward making in-house parts that are actually unprofitable. A common cause is that finance and production read the same ERP field with different interpretations.
How to improve it
Three levers, in the order they pay off:
- Measure automatically first. Without continuous automatic state capture, every improvement project aims at a moving target. Once the losses are visible they can be assigned to causes, and the first improvement targets become obvious. The Meleghy rollout across four plants produced 7 percent higher output in six months.
- Attack micro-stops. A Pareto of stops from one week of automatic data shows which few causes account for most of the lost minutes; fix those first.
- Structured SMED on changeovers.
Customer StoryAutomotive · PDF
How Meleghy Automotive connects its plants with a single MES platform
- −10 %downtime
- +7 %output
- 4 plantsin six months
 Case Study
FAQ
Is operating time the same as uptime?
No. Uptime is the raw powered-on clock value. Operating time excludes idle periods. A machine can be up for 8 hours and only producing for 6, giving 100 percent uptime but 75 percent operating time rate.
Does changeover count as operating time?
By the standard OEE convention, no. Changeover is a stop. Some plants book it as planned, some as unplanned, but either way it is outside operating time. The definition needs to be fixed once and held consistent across sites, otherwise cross-plant benchmarking is meaningless.
How accurate is manually recorded operating time?
It carries an upward bias. Stops below the manual logging threshold almost never get logged. Automatic capture records them as they happen.
What is a realistic target?
Do not set a target before measuring honestly for one quarter. The baseline that comes out of automatic capture is always more useful than a target imported from a benchmark sheet.
How fine should the resolution be?
The resolution has to be finer than the shortest stop you want to see, aggregated to shift or daily reports. Coarser capture misses micro-stops.
What software captures operating time automatically?
A modern MES or dedicated OEE platform that records machine states automatically, via OPC UA or, for older machines, via digital signals. Production metrics in SYMESTIC record quantities, scrap and downtimes automatically, and commissioning takes hours, with the first machine in under three hours.
Related: OEE · Machine Availability · Machine Runtime · Production Time · Machine Data Capture · MES · SYMESTIC Production Metrics
Potential analysis30 minutes · free
Calculate what your stops cost per year
In a free 30-minute call we take your stop times and calculate what they cost you per year.
In use in over 20 countries


Live demo30 minutes · free
See SYMESTIC on your own use case
In a free live demo, a product expert walks you through the running platform and shows what OEE, downtime and the connection of your machines and ERP look like in practice.
In use in over 20 countries

Use caseOEE software
Your OEE live, not in Excel at month-end
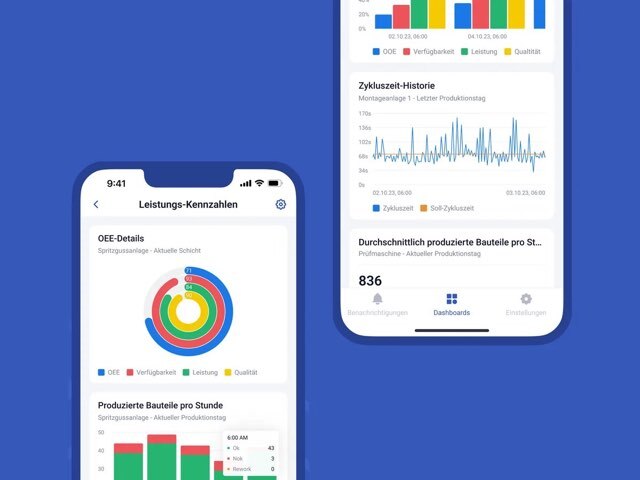
SYMESTIC measures availability, performance and quality right at the machine. The first machine is connected in under three hours, even an older one.
In use in over 20 countries

Six Sigma Black Belt with more than 25 years in manufacturing, previously at Johnson Controls, Visteon, iTAC and Dürr.
Book: „OEE: Eine Zahl, viele Lügen“ (2025)
- Manufacturing Execution Systems (MES)
- OEE
- Shopfloor Digitalization
- Six Sigma (Black Belt)
Updated
All articles by Christian Fieg