
Contents
What is SMED (Single-Minute Exchange of Die)?
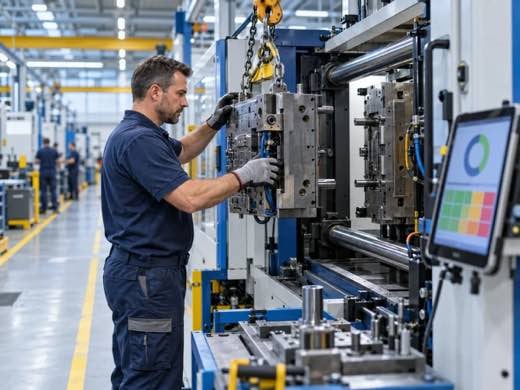
SMED, short for Single-Minute Exchange of Die, is a lean manufacturing method to reduce machine changeover time to less than ten minutes, which in Japanese is expressed as a single-digit number of minutes. The method was developed by Japanese industrial engineer Shigeo Shingo at Toyota and Mazda between 1950 and 1969, and it is the technical backbone of every modern pull system and small-batch production strategy.
Changeover time is measured from the last good part of the old product to the first good part of the new product at target speed and target quality. Everything in between counts, including the walk to the tool crib, the search for the torque wrench, the first-off inspection and any adjustments after the restart. This strict definition is what separates SMED from informal setup improvement exercises.
Analyze your changeover time with the SMED calculator
The economic logic is brutal. A press with a 90-minute changeover and 300 € per hour of production value loses 450 € in direct capacity per change. Cut the changeover to 9 minutes and the same machine runs smaller batches profitably, inventory drops, lead time shrinks and OEE rises. SMED does not just save time. It unlocks a completely different production economics.
Internal vs. external setup: the single most important distinction
Shingo's core insight was that setup work falls into two categories, and most plants mix them up constantly. Once you separate them, half of the improvement comes for free.
| Category | Definition | Typical examples | Status of machine |
|---|---|---|---|
| Internal setup (IED) | Tasks that can only be done when the machine is stopped | Removing the old die, bolting down the new die, loading a new program | Stopped, non-productive |
| External setup (OED) | Tasks that can be done while the machine is still running the previous order | Pre-heating the next die, staging tools, retrieving raw material, preparing the work order | Running, productive |
In an unimproved changeover, roughly 30 to 50 % of what operators do while the machine is stopped is actually external work that was simply postponed. That is pure, recoverable downtime.
The seven steps of a SMED project
Shingo's original method and its modern extensions boil down to seven concrete steps. They are sequential on paper and iterative in practice.
| Step | Activity | Typical time reduction |
|---|---|---|
| 1. Observe & measure | Video-record a full changeover, timestamp every activity, build the baseline | Baseline |
| 2. Separate internal and external | Classify each activity as IED or OED; move everything that can be OED out of the stopped window | 30–50 % |
| 3. Convert internal to external | Pre-heating, pre-assembly, quick-change fixtures that let preparation happen in parallel | Further 10–25 % |
| 4. Streamline internal tasks | Quick-release clamps, standardized bolt heights, zero-point clamping systems, one-turn fasteners | Further 10–30 % |
| 5. Streamline external tasks | 5S at the changeover cart, shadow boards, kitting, tool pre-staging | Operator effort |
| 6. Parallelize | Two operators on both sides of the machine, choreographed like a pit stop | 30–50 % of remaining time |
| 7. Standardize & sustain | Written standard work, LPA audits, MES-based monitoring of actual vs. target changeover | Prevents regression |
The benchmark from the original Toyota case is legendary: a stamping press changeover that reportedly took about four hours at Toyota dropped to a few minutes by 1969. Most of that came from steps 2 and 3, not from exotic hardware.
Beyond SMED: OTED and the modern tool landscape
Shingo himself later formulated One-Touch Exchange of Die (OTED) as the aspiration to cut changeover below 100 seconds, and No-Touch Exchange of Die (NTED) as fully automated tool changes. They are not marketing terms. CNC machining centres with automatic tool changers, IMM with quick-coupling systems and robotic die handling have made both realistic for a growing number of processes.
| Concept | Target changeover | Typical enablers |
|---|---|---|
| SMED | < 10 minutes | IED/OED separation, quick clamps, standard work |
| OTED | < 100 seconds | Zero-point clamping, hydraulic clamps, pre-heated dies |
| NTED | Operator-free | Robotic die change, automatic tool magazines, recipe-driven PLC |
For most mid-sized manufacturers, OTED on bottleneck equipment and disciplined SMED on everything else is the economically rational target. Full NTED only pays off on machines with very high changeover frequency.
How a cloud MES makes SMED real
Every SMED project starts strong and then quietly regresses. The root cause is almost always the same: nobody measures changeover time continuously, so the discipline erodes within six months. This is where a Manufacturing Execution System turns a workshop exercise into a permanent capability.
| SMED lifecycle stage | Manual / paper approach | With SYMESTIC MES |
|---|---|---|
| Baseline measurement | Stopwatch on one shift | Every changeover auto-measured from the last good part to the first good part via the machine signal |
| Target setting | Single number in Excel | Target changeover time per product |
| Deviation tracking | Detected in the next shift meeting | Exceeding the target is booked as its own downtime reason |
| Root cause analysis | Memory-based, fragmented | Process data and alarm logs tied to every setup event, queryable per article pair |
| KPI impact | Quarterly slide deck | Live OEE impact on the production KPI dashboard |
Meleghy Automotive achieved a 10 % reduction in downtime and a 7 % output improvement with SYMESTIC.
SMED in the real world: what the numbers look like
The gap between a good and a mediocre SMED programme is usually an order of magnitude. Three representative anchor points from mid-size European manufacturers:
| Process | Baseline | After SMED | Main levers |
|---|---|---|---|
| Stamping press, automotive | 120 min | 12 min | Quick-clamp die system, external pre-heating, two-operator choreography |
| Injection moulding, FMCG | 75 min | 18 min | Quick-coupling water/hydraulics, kitted tool cart, standardized recipes |
| Blister packaging, pharma | 55 min | 20 min | Format part pre-staging, no-tool format change, GMP-compliant cleaning parallelized |
FAQ
Does the "single minute" in SMED really mean under 60 seconds?
No. "Single minute" refers to a single-digit number of minutes, meaning less than ten. Sub-60-second changeovers are covered by the follow-on concept OTED (One-Touch Exchange of Die). The distinction matters in audits and coaching because setting a 60-second target on a press that today takes two hours demoralizes the team on day one.
Where does SMED show up in OEE?
In the Availability factor. Changeover time is planned downtime in some OEE definitions and unplanned in others, but in every credible calculation it counts against the machine. A plant that cuts a 90-minute changeover to 9 minutes on a machine with five changeovers per day recovers 6.75 hours. On a 16-hour day, that is a direct 42 % Availability uplift on top of whatever else OEE work delivers.
Do we need SMED if our changeovers are already short?
The test is economic, not absolute. If a changeover is short enough that lot sizes can be reduced without hurting capacity, and inventory is already where you want it, further SMED has diminishing returns. For most mid-sized manufacturers the opposite is true: lot sizes are kept artificially large because nobody has ever properly attacked changeover time, and finished-goods inventory absorbs the penalty.
How long does a SMED project take?
A structured kaizen event on a single machine typically runs one week: two days of observation and video analysis, two days of implementation and trials, one day of standardization. A 30 to 50 % reduction in this first pass is normal. Getting below ten minutes usually requires a second pass with hardware investments (quick clamps, zero-point systems). The sustaining layer, and this is where an MES earns its keep, is permanent.
Is SMED compatible with regulated industries like pharma?
Yes, with added discipline. GMP environments impose cleaning, line clearance and documentation steps that cannot simply be parallelized away. The SMED logic still applies: separate what can be external, choreograph what must be internal, and digitize the documentation so it stops being the bottleneck.
Related: Lean Production · Kaizen · Muda · Takt Time · Heijunka · TPM · OEE
Potential analysis30 minutes · free
Calculate what your changeovers cost per year
In a free 30-minute call we take your changeover times and frequency and calculate the lost capacity in euros.
In use in over 20 countries


Use caseReduce changeover time
Which changeover costs you the most time?
SYMESTIC measures every changeover automatically. The changeover matrix shows the slowest product changes at a glance.
In use in over 20 countries