Please fill in the required fields on the left to see your OEE result.
OEE formula: availability, performance and quality
OEE combines three factors measured over the same reporting period. Availability compares run time with planned production time. Performance compares actual output with output possible at the ideal cycle time. Quality counts first-time good parts.
In this calculator, scheduled time minus the entered planned exclusions gives planned production time. The unplanned downtime input then reduces run time. Include changeovers and setup time within planned production time as availability losses when production is scheduled. Record their minutes in that downtime field, even when the setup itself was planned.
| Measure | Formula | Unit or basis |
|---|---|---|
| Availability | Run time ÷ planned production time | Decimal factor A |
| Performance | Produced parts ÷ theoretical parts at ideal cycle | Decimal factor P |
| Quality | (Produced − scrap − rework) ÷ produced | Decimal factor Q |
| OEE | A × P × Q × 100 | % |
Worked example: OEE for a 480-minute shift
Illustrative inputs: 480 minutes scheduled, 30 minutes excluded before planned production time, 45 minutes downtime and a 30-second ideal cycle. Of 720 produced parts, 20 are scrap and 10 require rework.
| Measure | Calculation | Result |
|---|---|---|
| Planned production time | 480 − 30 | 450 min |
| Run time | 450 − 45 | 405 min |
| Theoretical parts | 405 × 60 ÷ 30 | 810 parts |
| Availability | 405 ÷ 450 | 90% |
| Performance | 720 ÷ 810 | 88.89% |
| Quality | 690 ÷ 720 | 95.83% |
| OEE | 0.90 × (720 ÷ 810) × (690 ÷ 720) | 76.67% |
Downtime cost scenarios and calculation limits
- Theoretical part counts are rounded down in the existing calculator. Performance is capped at 100%. If actual output exceeds the theoretical count, review ideal cycle time and counting boundaries before interpreting the result.
- The optional value scenario compares potential good output with actual good output and multiplies the gap by the contribution margin you enter. It includes availability, performance and quality losses. It is not a direct measurement of downtime cost or guaranteed recoverable revenue.
- For the example, potential good output is 900 parts. The gap to 690 good parts is 210. At an illustrative €5 contribution per part, the model value gap is €1,050 per reporting period. Fixed costs and actual demand are outside that scenario.
- Use the same first-pass outcome rules for scrap and rework so no part is deducted twice. OEE uses planned production time; TEEP additionally considers calendar utilization.
Calculation source: Lean Enterprise Institute: Overall Equipment Effectiveness. All worked-example inputs are illustrative.
How the OEE calculator works
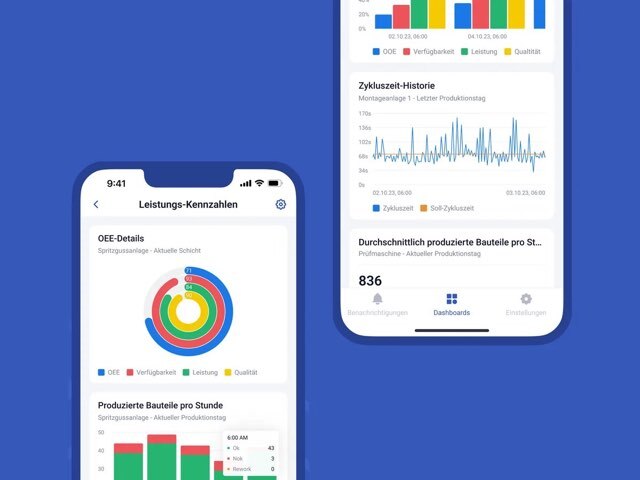
OEE (Overall Equipment Effectiveness) measures how productively a machine actually runs. In four steps you get your value – including the breakdown into Availability, Performance and Quality as well as the resulting loss in euros.
Frequently asked questions about OEE calculation
OEE (Overall Equipment Effectiveness) is the key metric for the productivity of a machine. It combines three factors – Availability, Performance and Quality – into a single percentage. 100 % OEE means: only good parts are produced, at maximum speed, with no downtime at all.
OEE = Availability × Performance × Quality. Specifically: Availability = operating time ÷ planned production time, Performance = (ideal cycle time × parts produced) ÷ operating time, and Quality = good parts ÷ parts produced. The three factors are expressed as percentages and multiplied together.
85 % is considered world-class. The average in discrete manufacturing is around 60 %. Values below 40–50 % are critical – but offer the largest and often quickly achievable improvement potential. The world-class target is made up of Availability ≥ 90 %, Performance ≥ 95 % and Quality ≥ 99.9 %.
OEE evaluates the planned production time. TEEP (Total Effective Equipment Performance) additionally factors in utilization and measures against the entire calendar time (24/7): TEEP = Utilization × OEE. TEEP therefore shows the maximum capacity potential of a machine – for example, whether an additional shift would pay off.
The six big loss categories are mapped to the three OEE factors: Availability – equipment breakdowns and setup/changeover losses; Performance – idling/minor stops and reduced speed; Quality – process defects/scrap and startup/rework losses.
Always start with the biggest loss. Availability: reduce setup times with SMED and establish preventive maintenance. Performance: eliminate minor stops and stabilize equipment speed. Quality: root-cause analysis, poka-yoke and a higher First Pass Yield reduce scrap and rework.
The hidden factory describes the capacity that goes unused because of OEE losses. At 60 % OEE, a second, invisible factory is effectively working against you. This capacity can often be recovered without additional investment, simply through a higher OEE – the calculator can quantify it in euros on request.
The required inputs are: total shift time, planned and unplanned downtime, ideal cycle time as well as parts produced, scrap and rework. Optional are the contribution margin per unit (for the euro valuation), the calendar time (for TEEP).