

Contents
Shop Floor Management (SFM) is a leadership method where managers lead from the production floor — not the office. It structures daily operations through tiered meetings (5–15 min per level), visual management boards, standardized escalation paths, and embedded problem-solving routines. SFM originated in the Toyota Production System and is now the operational backbone of Lean and CIP programs. The difference between SFM that stalls after 6 months and SFM that becomes permanent: real-time data. When the SFM board shows yesterday's OEE from an MES — not hand-written estimates — the meeting changes from storytelling to decision-making.
Transparency note: SYMESTIC is a cloud-native MES platform. Our dashboards are used as digital SFM boards by customers including Meleghy Automotive (4 plants) and Schmiedetechnik Plettenberg. Results cited are from approved implementations.
Table of contents
- What is shop floor management?
- What are the 5 pillars of SFM?
- How does the meeting cascade work?
- What belongs on an SFM board?
- Physical board vs. digital dashboard — which is better?
- How do you implement SFM step by step?
- Why do most SFM programs fail after 6 months?
- How does an MES support SFM?
- FAQ
What is shop floor management?
Shop Floor Management (SFM) is a leadership method in which managers lead directly from the production floor through structured daily routines: short tiered meetings, visual performance boards, standardized escalation paths, and embedded problem-solving. It is not a project or a tool — it is a daily operating rhythm.
The concept originates from the Toyota Production System (TPS) and the Japanese principle of Gemba (現場 — "the real place"). The core idea: management decisions improve when made at the point of value creation, not in a meeting room two floors up.
SFM connects three disciplines that are often managed separately: daily operations (shift handovers, capacity, order status), performance management (OEE, quality, throughput), and continuous improvement (CIP/Kaizen). The SFM board and the daily meeting are where all three converge.
What are the 5 pillars of SFM?
| # | Pillar | What it means | What kills it |
|---|---|---|---|
| 1 | Leadership on the Gemba | Managers spend 30–40 % of their time on the shop floor. Not inspecting — observing, asking, coaching. | Delegation to a "SFM coordinator" nobody listens to |
| 2 | Visual management | Performance, deviations, and actions are visible at a glance — on a physical board or digital dashboard | KPIs locked in management reports nobody reads |
| 3 | Structured communication | Tiered daily meetings (5–15 min per level), fixed time, fixed agenda, fixed escalation path | Meetings that expand to 45 min because structure is absent |
| 4 | Embedded problem-solving | Problems identified in the daily meeting enter a structured PDCA cycle — tracked on the board | Problems "noted" but never assigned, tracked, or verified |
| 5 | Employee involvement | Operators own the first meeting level. They present, they escalate, they track. Leadership enables. | Top-down meetings where the shift leader reads a report to silent operators |
How does the meeting cascade work?
The SFM meeting cascade is a tiered communication system where information flows upward from the shop floor and decisions flow downward — within the same morning.
| Level | Time | Duration | Participants | Content |
|---|---|---|---|---|
| L1: Team | 06:05 | 5–8 min | Team leader + operators | Safety, yesterday's KPIs (OEE, quality, output), today's plan, open actions, escalations to L2 |
| L2: Area | 06:30 | 10–15 min | Area manager + team leaders | Escalations from L1, cross-line issues, resource conflicts, maintenance priorities |
| L3: Plant | 07:00 | 10–15 min | Plant manager + area managers + support functions | Escalations from L2, plant-level KPIs, cross-functional decisions, weekly trends |
The cascade works only when it is fast. If L1 takes 25 minutes, L2 starts late, L3 is cancelled, and the system collapses. The discipline of time is the most important design parameter — more important than content perfection.
What belongs on an SFM board?
| Section | Content | Update frequency |
|---|---|---|
| Safety | Open safety actions, near misses, days since last incident | Daily |
| Quality | Scrap rate, quality complaints | Daily (auto from MES) |
| Delivery / Output | Plan vs. actual output, order status, on-time delivery | Daily (auto from MES) |
| Performance / OEE | OEE per line, availability, performance, top downtime reasons | Daily (auto from MES) |
| Actions / CI | Open PDCA cycles, Kaizen ideas, assigned actions with due dates | Updated in every meeting |
The board follows the SQDCP structure (Safety–Quality–Delivery–Cost–People) used in Lean manufacturing worldwide. Not every plant uses all five categories from day one — start with the 3 most relevant and expand.
Physical board vs. digital dashboard — which is better?
| Dimension | Physical whiteboard | Digital MES dashboard |
|---|---|---|
| Data freshness | Updated manually before the meeting — often outdated or estimated | Real-time, automatic — always current |
| Multi-site | Each plant has its own board — no cross-plant view | All plants on one platform — benchmarking built in |
| History | Yesterday's data wiped when today's is written | Full history — trends, week-over-week, shift comparisons |
| Preparation effort | 15–30 min per shift to collect and write data | Zero — data flows automatically |
| Engagement | Tactile, familiar — operators write on it | Depends on UX — touchscreen boards can match physical engagement |
| Best practice | Hybrid: digital screen for KPIs (auto), physical space for actions and notes (manual) | |
SYMESTIC implementation example: At Schmiedetechnik Plettenberg, SYMESTIC dashboards replaced the manual data preparation for SFM meetings entirely. Real-time cycle times, output, stoppages, and deviations are visible on shop floor screens. The result: faster problem identification, more stable processes, and — in the words of Technical Director Thorsten Manns — "a real-time transparency we simply didn't have before." ERP integration (InforCOM) ensures that order status flows bidirectionally, eliminating manual transcription between planning and shop floor.
How do you implement SFM step by step?
| Phase | Timeline | Focus | Deliverables |
|---|---|---|---|
| 1. Data foundation | Weeks 1–4 | Connect machines, establish automatic OEE/downtime capture via MES | Real-time dashboards with OEE, output, top-5 stoppage Pareto |
| 2. Pilot line | Weeks 3–6 | Start daily L1 meeting at one line. Define board content, meeting rules, time, participants. | First daily meetings running, team leader coached |
| 3. Cascade | Weeks 6–10 | Add L2 and L3 meetings. Define escalation rules: what goes up, what stays at the team level. | Full 3-level cascade running daily |
| 4. CI integration | Months 3–4 | Embed PDCA tracking on the board. Link improvements to measurable KPI changes. | Action list with due dates, before/after OEE comparison |
| 5. Scale & sustain | Ongoing | Roll out to additional lines/plants. Quarterly SFM maturity audits. Celebrate and share successes. | Cross-plant SFM benchmarking, standardized board layout |
Why do most SFM programs fail after 6 months?
SFM is easy to start and hard to sustain. Most programs start strong and fade within two quarters. The reasons are structural, not motivational.
| Failure pattern | What happens | How to prevent it |
|---|---|---|
| Data dies first | Manual data collection stops when pressure rises — the board goes empty | Automatic data from MES — the board is always current, with zero effort |
| Leadership retreats | Plant manager attends for 3 months, then stops — signal: SFM is optional | Non-negotiable: L3 meeting is in the plant manager's calendar, permanently |
| Actions without follow-up | Problems identified but never tracked to closure — team loses trust | PDCA tracker on the board with due dates, reviewed every meeting |
| Meetings expand | 15-min meeting becomes 30 min — schedule collapses, cascade breaks | Timer. Fixed rules: if it can't be resolved in 2 min, it's escalated, not discussed |
How does an MES support shop floor management?
An MES is the data engine behind digital SFM. It delivers the KPIs that populate the SFM board — automatically, in real time, without manual collection.
| SFM board section | MES data source | Value for the daily meeting |
|---|---|---|
| OEE & Performance | Automatic machine data collection (cycle times, stoppages, counts) | No debate about "what the OEE was" — the number is objective |
| Downtime reasons | Automatic downtime classification + operator confirmation | Pareto of yesterday's losses → today's priority is clear |
| Order status | ERP integration (InforCOM, SAP, Microsoft Dynamics NAV, Business Central) | Plan vs. actual visible without checking the ERP |
| Alerts | Threshold-based notifications (OEE below target, excessive scrap) | Problems flagged before the meeting — not discovered during it |
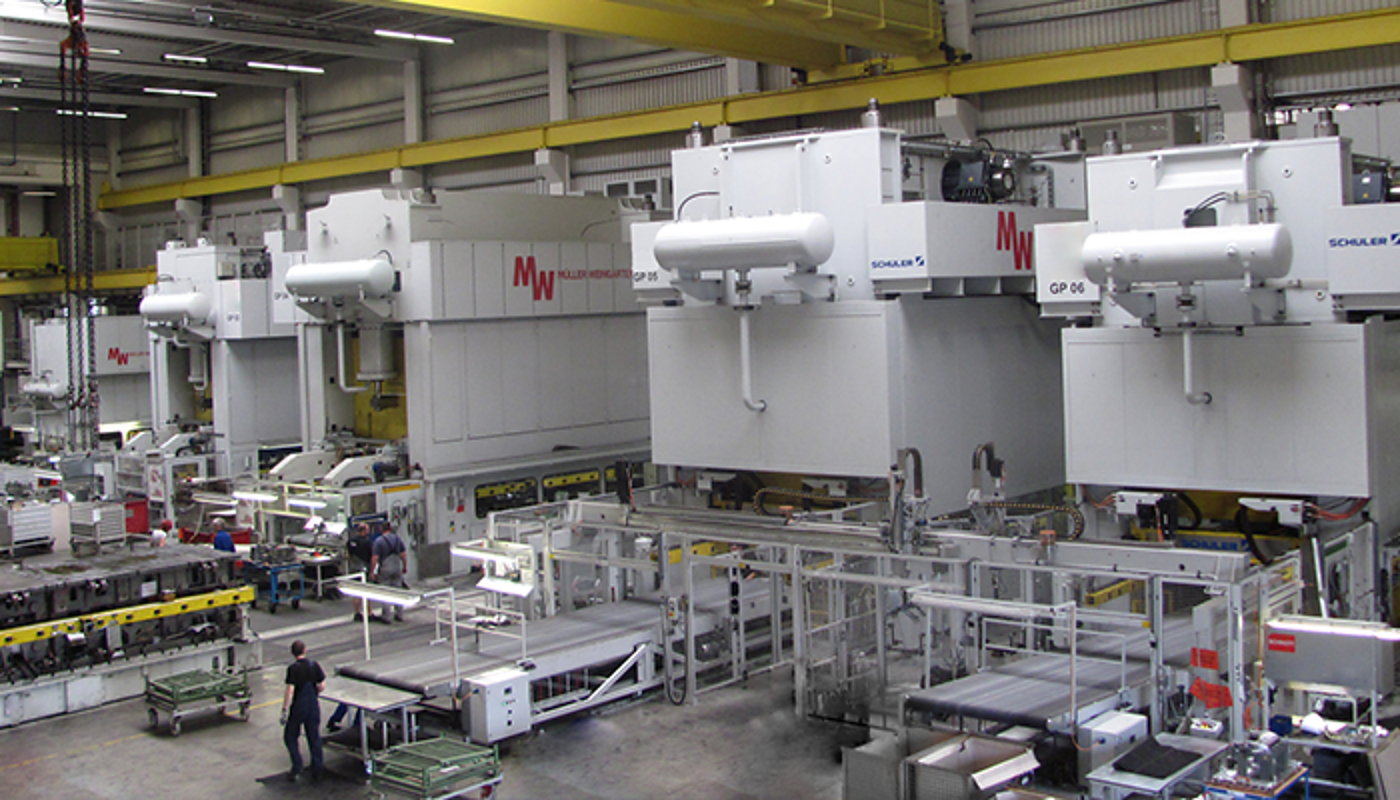
Multi-plant SFM with SYMESTIC: Meleghy Automotive runs SFM across 4 plants (Germany, Spain, Czech Republic, Hungary) on SYMESTIC. OEE data flows automatically from each plant into standardized dashboards. Bidirectional SAP R3 integration maps machine cycles to production orders. Results: 10 % fewer stoppages, 7 % higher output — across all plants, with the same data structure.

How Meleghy Automotive connects its plants with a single MES platform
- Standardized MES platform across all sites
- Real-time transparency in body production
- OEE & loss reasons captured automatically
- Scales from pilot to series production
 Case Study
FAQ
What is shop floor management?
Shop Floor Management (SFM) is a leadership method in which managers lead directly from the production floor through structured daily meetings, visual performance boards, standardized escalation paths, and embedded problem-solving. It originates from the Toyota Production System.
How long should an SFM meeting take?
The L1 (team) meeting should take 5–8 minutes. The L2 (area) meeting 10–15 minutes. The L3 (plant) meeting 10–15 minutes. If meetings regularly exceed these limits, the structure or escalation rules need redesign.
What is the difference between SFM and Lean?
Lean is the system-level framework for eliminating waste and creating flow. SFM is the daily management structure that makes Lean operational. Without SFM, Lean principles remain theoretical. Without Lean, SFM lacks strategic direction.
What KPIs belong on an SFM board?
The standard framework is SQDCP: Safety, Quality, Delivery, Cost, People. Most plants start with Quality, Delivery (output), and Performance (OEE) and expand over time. The key: fewer KPIs with real-time data beat more KPIs with stale data.
How does an MES support SFM?
An MES automatically populates the SFM board with OEE, downtime reasons, output, and order status — in real time. It eliminates manual data collection and ensures every meeting starts with facts, not estimates.
Can SFM work without digital tools?
Yes — many plants start with physical whiteboards and markers. This works for a single line or small plant. It breaks down at scale: multi-shift, multi-plant, or when manual data collection consumes more time than it saves. Most successful SFM programs transition to digital MES dashboards within 6–12 months.
The bottom line: Shop Floor Management is not a project to be completed — it is a daily rhythm that becomes the operating system of a production facility. The rhythm sustains when the data is automatic, the meetings are short, the escalation is clear, and the leadership is visible. Start with one line, one board, one meeting. The rest follows. A live demo shows the automatic data behind that first board.
→ What is an MES? · → OEE Explained · → CIP: Continuous Improvement · → Kaizen · → Lean Production · → Production Data Collection · → Operational Excellence
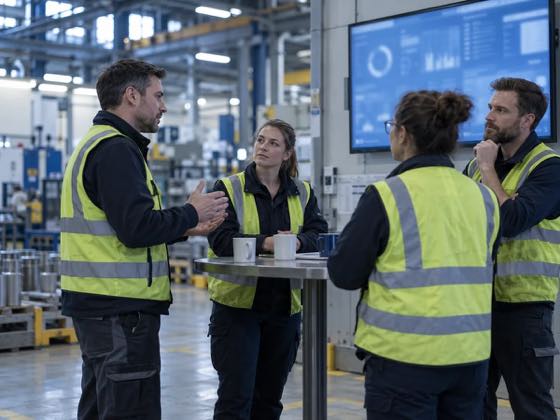
The shop floor board that fills itself
KPIs per line and shift come live from the machines. When a machine stops, the right people get a push notification.