




Contents
What is Muda?
Muda (無駄) is the Japanese word for waste — any activity that consumes resources without creating value for the customer. Taiichi Ohno, the architect of the Toyota Production System, identified 7 types of Muda in manufacturing. Every one of them is present in every factory. The question is not whether you have Muda — you do. The question is: can you see it? Because waste that is invisible cannot be eliminated. The customer pays for the machining, the assembly, the surface treatment. The customer does not pay for the 23 minutes the part sat in a buffer, the 4 minutes the operator walked to fetch a tool, or the 47 seconds the machine waited for a signal. That is Muda — and an MES is the system that makes it visible.
What are the 7 types of Muda and how do they show up in production data?
Ohno's 7 wastes are not abstract categories — each one maps directly to measurable losses in OEE, lead time, or cost. Here is how each waste appears on the shop floor and what the MES reveals about it:
| # | Waste (Muda) | What it looks like | OEE factor | How the MES makes it visible | Lean tool to attack it |
|---|---|---|---|---|---|
| 1 | Overproduction | Press runs 500 parts, only 400 ordered. 100 go to WIP inventory. | Consumes capacity — not directly in OEE but steals time from other orders | MES order tracking: produced quantity vs. ordered quantity. The gap is overproduction. | Kanban, JIT, pull-based scheduling |
| 2 | Waiting | Machine idle because material has not arrived, operator not available, upstream station still running. | Availability | MES logs idle time with reason code. Downtime Pareto: "waiting for material" as a top category. | Flow, line balancing, VSM |
| 3 | Transport | Parts moved 3 times between machining and assembly instead of flowing directly. | Not in OEE — extends lead time | MES order lead time analysis shows time-in-queue between operations. At Schmiedetechnik Plettenberg, real-time order tracking across machining chains made transport waste visible for the first time. | Cell layout, VSM, flow design |
| 4 | Overprocessing | Surface polished to mirror finish when customer spec requires matte. Or: deburring cycle runs 30 seconds, actual need is 18 seconds. | Performance (extended cycle time) | MES cycle time analysis: actual cycle time vs. standard. Consistently longer cycles without quality improvement = overprocessing. | Standard work, cycle time optimisation |
| 5 | Inventory | 3 weeks of WIP between stamping and welding. Raw material buffer for 6 weeks when supplier lead time is 2 weeks. | Not in OEE — ties up capital and hides other problems | MES order tracking: queue time per station shows where inventory builds up. High queue time = excess WIP. | Kanban, JIT, one-piece flow |
| 6 | Motion | Operator walks 20 metres to fetch tools every changeover. Reaches across the workstation 8 times per cycle. | Availability (extended changeover), Performance (extended cycle) | MES changeover time analysis shows variation across operators. High variation = non-standardised motion. SMED and 5S attack this. | 5S, SMED, ergonomic workplace design |
| 7 | Defects | 5 % scrap rate on injection moulding line. 20 parts reworked per shift on assembly. | Quality | MES scrap counter + reason code. Correlating alarm data with quality defects identifies root causes. | Jidoka, Poka-Yoke, SPC, root-cause analysis |
Ohno considered overproduction the worst waste — because it triggers all the others. Overproduction creates inventory, requires transport, hides defects (because they are discovered later, not immediately), and generates waiting (downstream stations are starved because upstream is producing the wrong product). An MES that shows real-time produced-vs.-ordered quantities at every station is the simplest and most effective overproduction countermeasure.
What is the 8th waste — and why does it matter more than the other 7?
The original 7 wastes focus on physical processes. Modern Lean practitioners add an 8th waste: unused human potential — the failure to use the knowledge, creativity and experience of the people who operate the machines.
This waste does not appear in machine data. But it is the root cause of why the other 7 wastes persist. When operators have no access to their own performance data, they cannot contribute to improvement. When shift leads receive OEE numbers 24 hours after the fact (if at all), they cannot act. When the CI manager must spend 2 hours collecting data from Excel spreadsheets before a Kaizen event can begin, the event starts with stale information.
The MES addresses the 8th waste directly: real-time dashboards on the shopfloor screen give operators the information they need to see waste as it happens — not in yesterday's shift report. At Schmiedetechnik Plettenberg, "all stakeholders — from shift leads to production management — gained a common, reliable view of running processes." That shared visibility is the antidote to unused human potential.
How does Muda relate to Mura and Muri?
Ohno did not see Muda in isolation. He defined three forms of production loss — the 3M:
| Japanese | English | Manufacturing example | How MES data reveals it |
|---|---|---|---|
| Muda (無駄) | Waste | Machine idle for 23 minutes waiting for material | Downtime Pareto with reason codes |
| Mura (斑) | Unevenness / variability | Press 3 runs at 95 % OEE on Monday and 62 % on Thursday. Same product, same operator. | OEE trend analysis per machine per shift: high variability = Mura. The SYMESTIC production metrics module shows this distribution automatically. |
| Muri (無理) | Overburden / strain | Machine running at 110 % of rated capacity to meet a deadline. Operator working double shifts for 3 weeks. | Process parameter monitoring: temperature, pressure, vibration above normal range = Muri on the machine. Alarm frequency increasing = machine under strain. |
The 3M are connected: Mura (unevenness) causes Muri (overburden during peaks) which causes Muda (breakdowns, defects, waiting during troughs). Attacking Muda alone — without addressing the variability that creates it — is treating symptoms. The MES makes all three visible: Muda in the downtime Pareto, Mura in the OEE variability chart, Muri in the process parameter alerts.
Why is most Muda invisible without an MES?
The fundamental problem: waste that takes less than 5 minutes is invisible to manual observation. An operator who walks 15 metres to fetch a tool does not log it. A micro-stop of 45 seconds does not appear in the shift report. A cycle that runs 3 seconds slow does not trigger an alarm. But 200 micro-stops per shift at 45 seconds each = 150 minutes of lost production. 3 seconds of cycle loss × 2,000 cycles per shift = 100 minutes of performance loss. These are not rounding errors — they are the difference between 65 % OEE and 80 % OEE.
The MES captures every cycle, every stop, every alarm — automatically, from the PLC signal, without operator input.
How do you systematically eliminate Muda?
| Step | Action | What happens | MES role |
|---|---|---|---|
| 1 | Make waste visible | Connect machines, capture OEE automatically, display real-time data on the shopfloor screen. | MES production metrics: automatic OEE, downtime reason codes, cycle time analysis. |
| 2 | Prioritise by impact | Downtime Pareto: what are the top 3 waste sources? Attacking the top 3 typically addresses 60–80 % of total loss. | MES Pareto chart ranks waste sources by total duration. |
| 3 | Analyse root cause | For each top waste source: why does it happen? Alarm correlation, process parameter analysis, 5-Why. | MES alarm history + process data trending. |
| 4 | Implement countermeasure | Kaizen event, SMED workshop, 5S action, standard work definition, spare-part stocking — depending on root cause. | MES provides baseline data before the countermeasure (the "C" in PDCA). |
| 5 | Verify and sustain | Did the countermeasure work? Is the improvement holding after 2 weeks, 4 weeks, 3 months? | MES trend comparison pre/post. At Meleghy, 10 % downtime reduction verified through MES data across 4 plants over 6 months. |
The most common failure: companies jump to step 4 (implement) without step 1 (make visible). They run a SMED workshop without knowing the actual changeover time. They implement 5S without knowing which motion wastes consume the most time. They install Kanban without knowing the actual consumption rate. Without data, Lean tools are applied to the wrong problems — and the improvement does not last because nobody can verify whether it worked. The MES provides the foundation: step 1 comes first, and it never stops. The most consistent way to remove waiting between stations is one-piece flow.
FAQ
Is Muda always bad?
Not all Muda can or should be eliminated. Lean practitioners distinguish between Type 1 Muda (non-value-adding but necessary — e.g., changeovers, quality inspections, transport to the next station) and Type 2 Muda (non-value-adding and unnecessary — e.g., overproduction, waiting, defects). Type 2 is pure waste to be eliminated. Type 1 is waste to be minimised: you cannot eliminate changeovers, but you can reduce them from 45 minutes to 15 minutes with SMED. The MES measures both types — and the distinction becomes clear in the data.
How does Muda relate to OEE?
OEE is the quantified sum of Muda on a machine. Availability losses (downtime, changeovers) = waiting Muda + motion Muda. Performance losses (slow cycles, micro-stops) = overprocessing Muda. Quality losses (scrap, rework) = defect Muda. When OEE is 65 %, the remaining 35 % is Muda — measured, categorised and ready for elimination. That is why OEE is the primary Lean metric on the shopfloor: it translates Ohno's philosophy into a number that operators can act on every shift.
Can you eliminate all Muda?
No. Perfection is the direction, not the destination — that is Lean Principle 5 (Pursue Perfection). Every improvement reveals the next layer of waste that was previously hidden. A plant at 85 % OEE has eliminated the gross waste. The remaining 15 % is harder, subtler and more expensive to address. The MES helps here too: as obvious waste is eliminated, the data reveals the next tier — micro-stops that were invisible when major stops dominated the Pareto, cycle time variations that were noise when the machine was down 30 % of the time.
What is the fastest way to start reducing Muda?
Connect 10 machines to an MES. Display OEE in real time on the shopfloor. Hold a 15-minute daily shopfloor meeting in front of the dashboard. Ask one question: "What was the biggest waste source yesterday and what will we do about it today?" That is not a 6-month Lean transformation project. It changes behaviour from day one, because for the first time, everyone can see the waste.
Related: Lean Management · Lean Production · Kaizen · Kanban · Value Stream Mapping · 5S Method · SMED · Jidoka · OEE Explained · MES: Definition & Functions · Shopfloor Management
Excel templateFree download
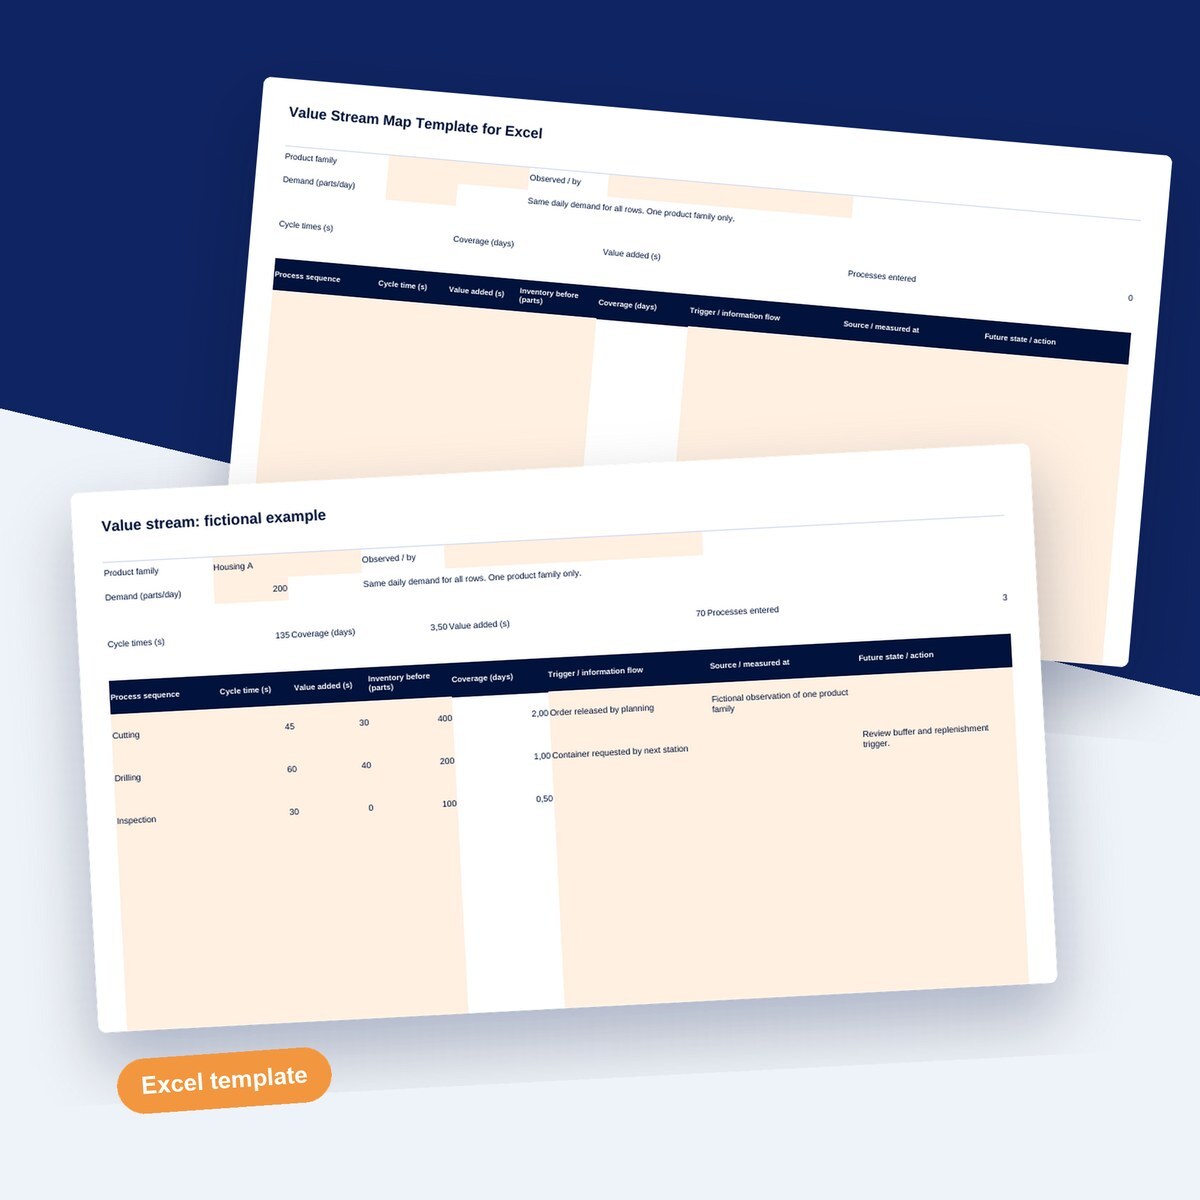
Value stream map: Excel template
Use this template to capture one product family from the first process to the last and record cycle time, inventory and information flow separately.
- Current-state process sequence with cycle time and inventory before each process
- Inventory coverage from inventory and daily demand, calculated by formula
- Cycle time, value-added time and coverage in separate units
Excel template
Value stream map: Excel template
- Current-state process sequence with cycle time and inventory before each process
- Inventory coverage from inventory and daily demand, calculated by formula
- Cycle time, value-added time and coverage in separate units

Six Sigma Black Belt with more than 25 years in manufacturing, previously at Johnson Controls, Visteon, iTAC and Dürr.
Book: „OEE: Eine Zahl, viele Lügen“ (2025)
- Manufacturing Execution Systems (MES)
- OEE
- Shopfloor Digitalization
- Six Sigma (Black Belt)
Updated
All articles by Christian Fieg